
Quick answer: A medical equipment enclosure gap-and-flush specification should define the nominal gap, permitted gap variation, permitted flush offset, measurement locations, cosmetic surface class, assembly state, support condition, finish condition, and inspection method for every critical visible seam. There is no universal “medical enclosure panel gap” that suits every product. The correct value depends on enclosure size, sheet thickness, forming and welding route, hinge and latch design, gasket compression, coating, service requirements, industrial design, and the OEM’s risk-based acceptance criteria.
MSTFAB manufactures unpopulated custom sheet metal enclosure shells and mechanical parts from buyer-approved drawings. Our scope can include bodies, doors, removable covers, mounting plates, brackets, hinges, latches, studs, mechanical hardware, welding, finishing, gap-and-flush inspection, first-article records, and export packaging. We do not manufacture finished medical devices, install medical electronics, validate clinical performance, define regulatory requirements, or certify the completed equipment.
A panel can be dimensionally correct and still look wrong from across the room. One seam grows from 2.5 mm to 4.0 mm. A removable cover sits 1 mm proud at one corner. A door is aligned while open but drops after the buyer installs a display and handle. The enclosure remains functional, yet the product now appears as though several departments designed it without being introduced.
For medical, laboratory, and aesthetic equipment, visible enclosure alignment influences perceived quality, cleaning access, service fit, labeling position, and confidence during customer acceptance. It is not a medical certification by itself. It is a controlled mechanical characteristic that should be designed, manufactured, measured, and approved like any other critical interface.
What Do Gap and Flush Mean on a Medical Enclosure?
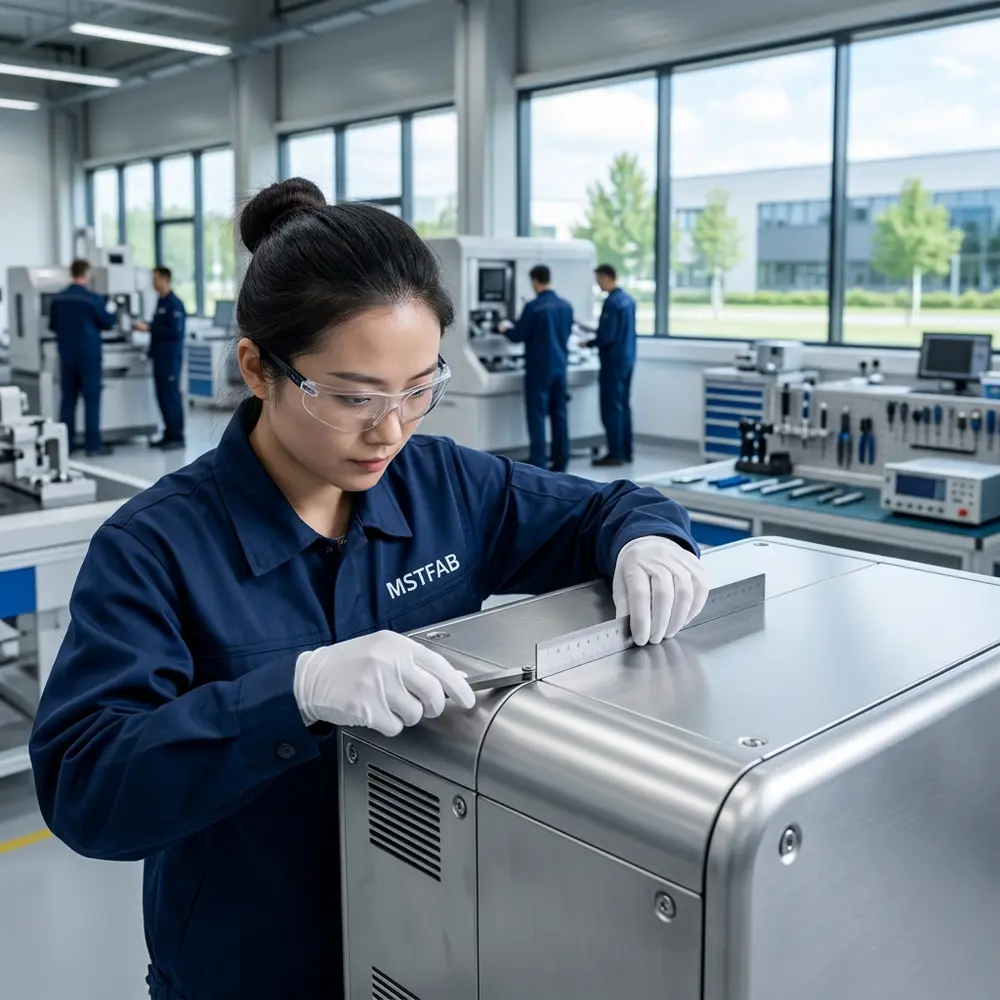
Panel gap is the visible distance between two adjacent edges, measured at specified positions and in a specified assembly condition. Flush, also called flushness or step, is the height difference between the adjacent surfaces in the direction normal to the intended exterior surface. A seam can have the correct gap and the wrong flush offset, or the correct flush offset and a gap that changes from top to bottom.
| Characteristic | What the drawing should define | Common misunderstanding |
|---|---|---|
| Nominal gap | Target distance between the selected panel edges | “Keep the gap small” is not a measurable target |
| Gap variation | Permitted range or change between defined measurement positions | One acceptable reading does not prove a parallel seam |
| Flush offset | Permitted positive and negative step between adjacent finished surfaces | A consistent gap can still join two visibly stepped panels |
| Alignment or continuity | Relationship of body lines, corners, radii, grain, graphics, or feature edges | Matching overall panel size does not align the visible architecture |
| Inspection condition | Latched or unlatched state, gasket state, support plane, installed hardware, finish, and load | The same enclosure can measure differently on a twisted pallet and a level base |
| Surface class | Which seams are customer-facing, service-facing, hidden, or non-cosmetic | Applying showroom criteria inside every service compartment increases cost without adding value |
Gap is not the same as clearance
A visible gap is part of the exterior architecture. Functional clearance is the space required for movement, assembly, coating, gasket compression, or service. They may influence one another, but they are not interchangeable. A designer may want a narrow visual seam while the hinge path needs more movement clearance behind it. The drawing must resolve both conditions.
Flushness is not general panel flatness
Panel flatness describes variation across one surface. Flushness compares adjacent surfaces at a seam. A large door can have local oil-canning away from the seam while still meeting the specified edge flushness. Conversely, two individually flat panels can sit at different heights because their locating brackets or fasteners disagree.
There is no universal medical-device gap tolerance
No single nominal gap or flush tolerance should be copied into every medical enclosure drawing. A compact diagnostic housing, a floor-standing imaging console, and a mobile treatment cart have different dimensions, loads, finishes, service access, and manufacturing routes. The OEM should set acceptance from product architecture, user expectations, mechanical stack-up, risk, and validated design inputs.
Where a company uses geometrical product specification or GD&T practices, the drawing team may reference an applicable standard such as ASME Y14.5 Dimensioning and Tolerancing. The standard supports clear engineering communication; it does not select a cosmetic gap for the product.
Why Gap and Flush Matter to Medical Equipment Buyers
Perceived quality begins before the machine is switched on
Operators, distributors, service technicians, and purchasing teams often see the enclosure before they understand the technology inside it. Consistent seams, aligned corners, and stable panel planes signal process control. Uneven gaps can make expensive equipment look improvised even when the internal engineering is excellent. It is unfair to the electronics, perhaps, but the electronics rarely attend the sales demonstration alone.
Cleaning access and cosmetic alignment are related but separate
A narrow, inconsistent seam may trap residue or make wiping difficult, but cleanability depends on actual cleaning exposure, joint design, hardware, radii, finishes, and approved cleaning agents. This article owns dimensional gap-and-flush specification and inspection. Detailed crevice and wipe-access decisions remain in the medical enclosure cleanability DFM guide and the cleanability and cosmetic finish checklist.
Service panels must look aligned and remain removable
A removable cover needs enough clearance to install and remove after finishing, but excessive float can create visible drift. Locating features should establish position; fasteners should clamp the panel. Asking clearance holes to locate the cover makes the final alignment depend on whichever side of each hole the assembler happened to meet that morning.
Gap and flush are not regulatory approval
An aligned enclosure shell is not a medically certified product. The legal manufacturer or responsible OEM owns device classification, design inputs, risk management, usability, cleaning validation, electrical safety, clinical performance, labeling, and applicable quality-system obligations. In the United States, buyers should review the current FDA Quality Management System Regulation information with qualified regulatory professionals. A fabricator’s dimensional report is useful supplier evidence, not a substitute for the finished device manufacturer’s responsibilities.
Responsibility Matrix for Gap-and-Flush Quality
| Decision or activity | Responsible owner | Expected output |
|---|---|---|
| Industrial design, intended appearance, user-facing seam map, and service concept | Medical equipment OEM or design owner | Approved product architecture and surface classes |
| Nominal gaps, flush limits, datum scheme, measurement positions, and acceptance state | OEM mechanical engineering and quality teams | Released drawings and inspection specification |
| Cutting, bending, welding, hardware installation, finishing, mechanical assembly, and packaging | MSTFAB within buyer-approved drawings | Unpopulated fabricated enclosure shell and agreed records |
| Manufacturing DFM and process-risk feedback | MSTFAB with buyer approval for design changes | Documented questions, proposed process controls, and approved deviations |
| Installed electronics, displays, batteries, handles, accessories, cables, and final operating loads | OEM or final equipment assembler | Configured finished equipment and final fit confirmation |
| Medical-device conformity, validation, labels, release, and regulatory claims | Legal manufacturer and authorized specialists | Applicable product-level records and approvals |
This boundary does not mean the sheet metal supplier ignores appearance. MSTFAB can review manufacturability, recommend locating strategies, design fixtures for approved geometry, measure finished seams, and document first-article results. We simply do not invent the OEM’s product requirement or declare a finished medical device compliant because two covers line up nicely.
Build a Gap-and-Flush Specification Before the RFQ
Create a seam map
Mark every visible joint on the enclosure assembly: door-to-frame, cover-to-body, side-panel-to-front-panel, removable bezel, base skirt, top cap, HMI surround, and accessory panel. Give each seam an identifier such as G01 or F03 so the drawing, FAI report, photographs, and nonconformance record refer to the same location.
Classify visible surfaces and viewing zones
Define primary customer-facing surfaces, secondary service-facing surfaces, internal panels, and hidden construction. Then assign appropriate cosmetic and dimensional controls. A seam beside a user display may deserve tighter visual continuity than a removable rear service cover. A specification that calls every surface “Class A” usually means no one has decided which surfaces matter most.
State nominal values and permitted variation
For each critical seam, specify the nominal gap and tolerance or permitted range. If taper matters, define the maximum difference between measurement points. For flush offset, define the acceptable positive and negative step and establish which surface is the reference. Avoid phrases such as “even gap,” “perfectly flush,” or “premium medical appearance” unless they are followed by measurable criteria.
Define measurement positions
Long doors and covers can vary along their length. A single reading at the center may miss a large corner error. Identify measurement points by distance from corners, hinges, latches, or other stable references. For a vertical door seam, the inspection plan might require readings near the top, center, and bottom while excluding a small distance around formed radii. The exact positions belong on the drawing or inspection sheet.
Specify the finished assembly state
State whether the door is latched, whether all fasteners are torqued, whether the gasket is installed and conditioned, whether protective film is present, and whether the assembly is finished or bare. Specify any buyer-supplied hardware or representative load needed for acceptance. Otherwise, one team measures an empty unlatched shell while another judges a loaded finished unit. Both measurements can be honest and mutually useless.
Establish Datums and the Inspection Support Condition
Gap-and-flush results depend on what locates the panels and how the enclosure is supported. A floor-standing cabinet can twist when placed on an uneven pallet. A mobile enclosure can change after casters and ballast are installed. A wall-mounted housing may settle differently when held vertically rather than lying on an inspection table.
Use product-relevant datums
Useful cosmetic datums may include the finished base mounting plane, primary welded frame, front opening, hinge axis, or a controlled locating feature. Do not dimension every visible edge from unrelated bends. The datum strategy should connect the structure that controls panel position to the seam being inspected.
Separate locating from fastening
Use tabs, pilots, shoulders, slots, nests, pins, or other approved locating features where repeatable position matters. Fasteners provide clamp load. Oversized holes without locating intent permit the panel to wander; very tight holes can prevent assembly after coating. A robust design gives each feature one clear job instead of asking a screw to be locator, clamp, cosmetic stylist, and emotional support.
Define the support plane
Inspect on the specified base, level fixture, caster configuration, mounting bracket, or simulated installation plane. Record leveling or clamping requirements. If a large enclosure is sensitive to floor condition, the OEM should distinguish free-state acceptance from installed-state adjustment.

Design fixtures from the visible architecture
A welding fixture should prioritize door openings, panel interfaces, base geometry, and critical locating features. Holding every loose part firmly does not guarantee the right finished relationship. Fixtures also require identification, maintenance, and periodic verification; a worn fixture can repeat an error with admirable consistency.
Understand the Gap-and-Flush Tolerance Stack
The finished seam is rarely controlled by one dimension. It is the result of multiple contributors: material thickness, bend position and angle, frame squareness, weld distortion, hinge location, hinge play, latch pull-in, gasket compression, panel stiffness, fastener position, coating build, assembly sequence, and the final support plane.
A useful DFM review traces the complete stack from the structural datum to both adjacent finished surfaces. The goal is not to assign the tightest possible tolerance to every contributor. It is to control the few contributors that dominate the visual result and provide adjustment only where adjustment is intentionally designed.
| Variation source | Practical control | Evidence to review |
|---|---|---|
| Bend position and angle | Use achievable drawing tolerances, suitable tooling, bend sequencing, and in-process checks | Formed-part measurements and first-article assembly fit |
| Weld distortion and frame squareness | Control joint design, weld sequence, heat input, fixture datums, and post-weld inspection | Finished frame diagonals, opening dimensions, and fixture records |
| Hinge location, play, and installed load | Freeze hinge part number, mounting pattern, axis relationship, reinforcement, and representative door load | Door sweep, sag, gap readings, and loaded fit trial |
| Latch pull-in and gasket compression | Define latch position, adjustment, closing force, compression target, and inspection state | Latched gap-and-flush readings and approved setup |
| Removable panel float | Add approved locating features and manage hole clearance intentionally | Repeated remove-and-install trial and corner measurements |
| Coating and masking | Design clearance for the specified finish and inspect after the final coating route | Coating records, edge fit, and finished assembly results |
| Transport and handling | Restrain doors and panels, support the frame, and protect visible surfaces | Packaging approval and receiving-condition check |
Avoid defaulting to tighter tolerances everywhere
Tight overall tolerances can increase machining, fixture, inspection, and rejection costs without controlling the seam. If hinge position and latch compression dominate the gap, tightening a hidden rear flange may contribute very little. Define CTQs from the visible and functional stack, then leave reasonable manufacturing tolerance elsewhere.
Use adjustment only where it can be controlled
Slots, shims, adjustable hinges, and latch adjustment can help during assembly. They can also create variation if there is no setup instruction, adjustment range, tightening sequence, or inspection record. Adjustment is a design feature, not a permission slip for indefinite fitting.
Control Doors, Hinges, Latches, and Removable Covers
Evaluate the complete door geometry
Door width and height are not enough. Review edge returns, reinforcement, hinge axis, latch position, gasket land, installed display or handle cutouts, center of gravity, service opening angle, and neighboring panels. Large HMI openings can reduce stiffness and change local flatness; those details belong in the medical automation enclosure HMI cutout DFM guide.
Test with representative door loads
An empty door may align in the sheet metal factory and sag after the OEM installs a touchscreen, handle, cable chain, shielding, or internal bracket. The buyer should provide a representative mass, center of gravity, or mechanical dummy when the configured load affects alignment. MSTFAB can test the mechanical condition defined by the buyer; we do not select or validate the medical electronics.
Control hinge identity and axis
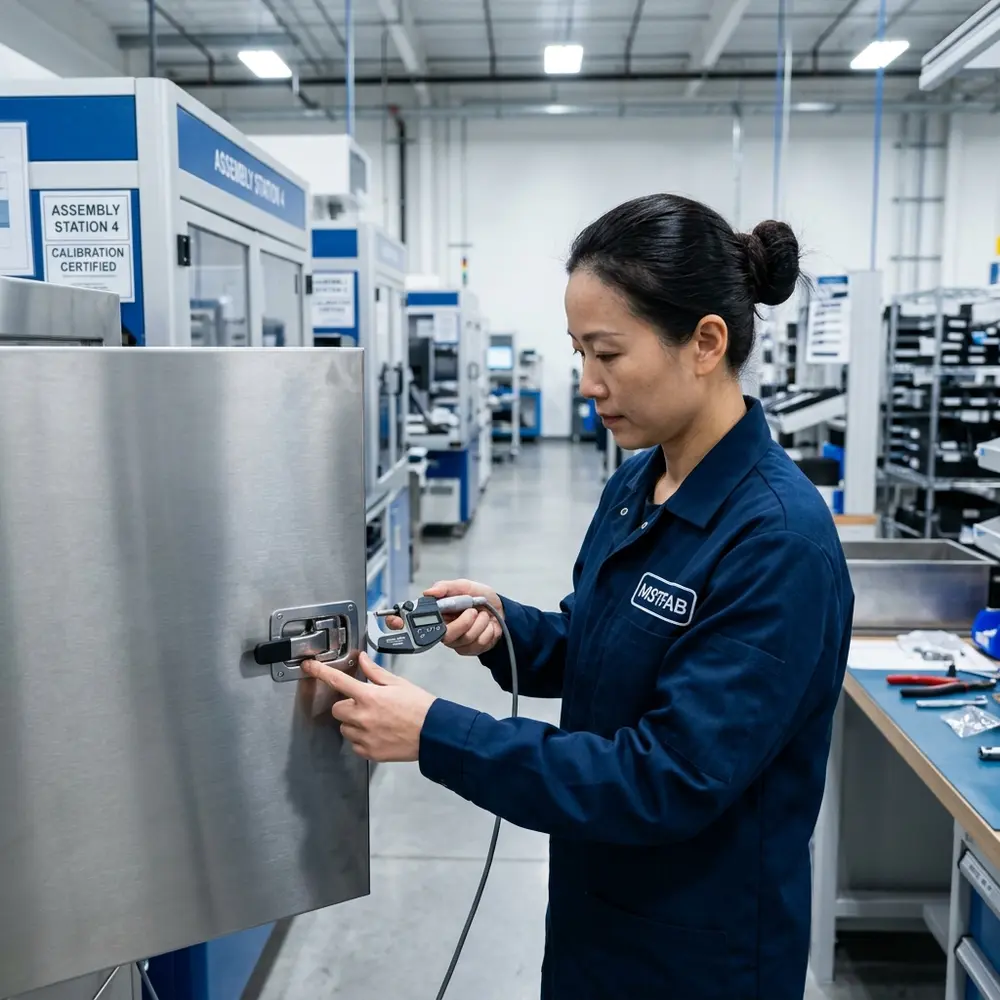
Freeze the hinge manufacturer, part number, pin clearance, material, mounting method, and approved alternatives. Small changes in leaf thickness or hole pattern can move the door. For concealed hinges, inspect both closed alignment and the opening path. For welded hinges, measure after the heat-producing operation that can move the axis.
Define latch pull-in and gasket state
Latches pull the door toward the frame and may compress a gasket. Too little pull-in can leave a proud edge; too much can bow a thin door or create uneven flushness between latch and hinge sides. The responsible OEM defines the gasket and closing requirement. The fabrication package defines the mechanical latch position, adjustment, and inspection state.
Give removable covers repeatable locating features
Repeatedly remove and reinstall a service cover during first-article review. If its alignment changes materially after each cycle, the design relies too heavily on operator judgment. Pilot tabs, locating shoulders, controlled slots, or other approved features can make service reassembly predictable while preserving the required clearance.
For detailed internal access and mounting-plate sequence, use the medical enclosure service-access DFM guide. For inserts and studs that influence cover position, use the medical enclosure PEM hardware DFM guide.
Inspect After Coating and Final Mechanical Assembly
Powder coating changes edge conditions
Powder coating adds material to both sides of a narrow seam and can build differently around edges, corners, holes, and recessed features. It can also influence hinge seating, threaded interfaces, panel sliding, and latch adjustment. The exact result depends on the approved coating system and geometry, so design and approve the finished condition.
For coating-system and pretreatment capabilities, see sheet metal surface treatment. The OEM should define the required coating, color, texture, cosmetic zones, masking, and environmental performance. A fabricator can manufacture and document the finish; material or coating choice alone does not make an enclosure suitable for a medical application.
Brushed stainless alignment includes grain continuity
On brushed stainless steel, adjacent panels may meet the dimensional gap requirement while appearing misaligned because grain direction, reflectivity, or weld blending differs. Control grain orientation and visible surface class separately from gap-and-flush dimensions. The brushed stainless enclosure finish guide owns the deeper surface-finish topic.
Approve the intended production process
If the prototype was hand-fitted, selectively shimmed, or refinished outside the planned process, document what must return to the drawing, fixture, or work instruction before production. A prototype that fits only because one talented technician remembers three invisible adjustments is not yet a repeatable manufacturing process. It is a live performance.
How to Measure Gap and Flush Repeatably
The inspection method should match the tolerance, surface risk, and production volume. The drawing or inspection plan should identify the tool, measurement points, assembly condition, resolution, and reporting rule. The equipment should be suitable and calibrated under the buyer’s agreed quality requirements.
Gap gauges and feeler gauges
Tapered gap gauges, pin gauges, leaf-type feeler gauges, or custom go/no-go gauges can measure or screen gaps depending on geometry and access. Avoid forcing a gauge into a coated seam, which can damage the edge or spread flexible panels. Record the method because different tools can produce different results on chamfered or rounded edges.
Straightedges, step gauges, and indicators
A precision straightedge with feeler gauges can screen flush offset across adjacent panels. A dedicated step gauge, depth gauge, or indicator fixture can provide more direct results where the tolerance requires it. Define the contact locations so the reading is not distorted by a formed radius, local texture, or oil-canning away from the seam.
Fixtures and digital inspection
For repeat products, a checking fixture can establish support and datum conditions while presenting defined gauge locations. Coordinate measurement, scanning, or digital profilometry may support complex geometry, but the result is only useful when the datum alignment and evaluation rule match the drawing. More decimal places do not repair an ambiguous requirement; they simply make the ambiguity look expensive.
Photographs support evidence but do not replace measurement
Photographs are valuable for showing overall appearance, seam continuity, and approved viewing conditions. They are sensitive to lighting, angle, lens distortion, and distance. Use photos with dimensional records rather than asking a close-up image to prove a 0.5 mm flush limit by personality alone.
First-Article Approval and the Golden Sample
The first article should establish whether the released design, production route, finish, hardware, assembly sequence, and inspection method produce the intended gap-and-flush result. It should be evaluated in the defined support and assembly condition before volume production.
What the gap-and-flush FAI should include
- part numbers, drawing revisions, and enclosure configuration;
- seam identifiers and measurement-point map;
- nominal gaps, tolerances, flush limits, and measured results;
- inspection tools, fixture, support plane, latch state, gasket state, and installed loads;
- material, finish, hardware, and approved deviations;
- photographs from controlled overall and detail views;
- reviewer, disposition, approval date, and production-release decision.
Use the golden sample as a visual reference
A golden sample can help teams compare overall seam architecture, texture, color, and acceptable appearance. It should not replace released drawings or measurable limits. Samples age, coatings fade, hardware loosens, and shipping leaves opinions. Identify, protect, date, and periodically review any retained reference sample.
Keep broader supplier handoff on its own page
This article owns gap-and-flush evidence. Material traceability, supplier change notification, deviation control, record retention, and broader repeat-batch quality planning remain in the medical enclosure supplier quality handoff guide. Linking the topics gives buyers a complete workflow without making two pages compete for the same query.
Repeat Production and Change Control
Repeat production needs the same support plane, hardware, fixture logic, assembly sequence, latch setting, finish route, measurement points, and acceptance rule used for the approved first article. A later batch can drift even when no single drawing dimension appears to have changed.
Trigger documented review when changing:
- sheet material, thickness, temper, or protective finish;
- bend tooling, bend sequence, weld sequence, or welding fixture;
- hinge, latch, gasket, fastener, insert, stud, or supplier part number;
- door reinforcement, cutout, handle, display, or configured door load;
- panel locating feature, clearance hole, slot, shim, or assembly order;
- powder, pretreatment, coating supplier, masking, or cure process;
- inspection fixture, gauge, support method, or measurement program;
- packaging restraint, pallet support, stacking, or transport orientation.
MSTFAB should not silently “improve” a critical seam by changing approved geometry. Proposed changes should be documented and accepted by the buyer before implementation. Likewise, buyer-requested changes should arrive through a released revision rather than an annotated photograph whose filename ends in “final_final2.”
Packaging Must Preserve the Approved Alignment
A good enclosure can arrive with a poor gap after a long export journey if doors swing, frames twist on the pallet, removable covers rub, or heavy accessories load the structure. Packaging is part of cosmetic and dimensional preservation.

Restrain doors without distorting them
Use approved latching, soft restraints, blocks, or supports that prevent movement without applying harmful point loads. Protect handles, hinges, and protruding features. If transport uses the product’s latch, confirm the gasket and latch will not take a damaging long-term compression set under the selected packing method.
Support the frame at intended load points
Pallet design should support the base or mounting points without twisting the structure. Large cabinets may need internal bracing or removable transit supports. Mark any support that the final assembler must remove before acceptance measurement.
Verify the receiving condition
For critical equipment, define a receiving check with photographs and selected gap-and-flush readings before electrical integration. This distinguishes manufacturing variation from transport damage and prevents a month of email in which everyone studies the same crooked door from different time zones.
RFQ and Drawing Checklist for OEM Buyers
| RFQ input | Minimum information | Buyer decision enabled |
|---|---|---|
| Controlled design package | Matching STEP assembly and dimensioned PDFs with revision | Review complete panel relationships and quote the correct configuration |
| Seam and surface map | Critical seam IDs, surface classes, viewing zones, and hidden areas | Apply effort where appearance and function matter |
| Gap-and-flush limits | Nominal gap, permitted variation, flush offset, and alignment criteria | Plan tolerances, fixtures, adjustment, and inspection |
| Inspection state | Support plane, orientation, finish, latch, gasket, torque, load, and measurement points | Compare supplier and buyer results under the same condition |
| Materials and hardware | Material grade, thickness, hinge, latch, gasket, inserts, fasteners, and approved alternatives | Control the components that influence panel position |
| Finish requirements | Coating or grain direction, masking, cosmetic acceptance, and cleaning exposure | Allow for finished fit and visible continuity |
| FAI and repeat control | Sample size, report format, tools, golden sample, approval, and change notification | Release production with traceable evidence |
| Commercial and logistics data | Prototype quantity, annual volume, delivery destination, packing, and configuration mix | Select a realistic production and export plan |
For a broader custom-enclosure capability review, see custom medical and aesthetic equipment enclosure fabrication. MSTFAB quotes and manufactures the sheet metal scope defined in the buyer’s released package; the OEM remains responsible for the finished equipment and its intended medical application.
Three Practical Gap-and-Flush Scenarios
Scenario 1: Floor-standing diagnostic console with a long front door
The door aligns when empty but drops after a touchscreen, inner bracket, and handle are installed. The solution is not automatically a tighter door-width tolerance. The OEM provides the representative load and center of gravity; the DFM review checks hinge axis, reinforcement, frame opening, latch pull-in, and service angle. First-article measurements are taken with the defined load and the enclosure supported on its approved base.
Scenario 2: Powder-coated aesthetic machine with four removable covers
Each cover uses generous clearance holes for easy service, so the cross-shaped seam at their intersection changes every time technicians reinstall them. The approved redesign gives the panels repeatable locating features while retaining installation clearance. The FAI includes three remove-and-install cycles and records corner gaps after each cycle. The screws return to their proper role as clamps and seem relieved by the reduced responsibility.
Scenario 3: Brushed stainless laboratory enclosure
Measured gaps pass, but adjacent covers look misaligned under overhead lighting because grain direction and surface reflection differ. The drawing separates dimensional seam requirements from grain orientation and cosmetic surface acceptance. Production protects the visible grain through fabrication and packing, while final gap-and-flush inspection remains a separate record.
Red Flags in Supplier or Drawing Language
- “Standard medical gap.” Ask for the source, product configuration, nominal value, tolerance, and inspection state.
- “Perfectly flush.” Replace the adjective with a signed flush limit and measurement method.
- “Supplier to ensure premium appearance.” Define surface classes, seams, viewing rules, and measurable CTQs.
- “Inspect before coating.” Use in-process checks as needed, but approve the seam after the finish that changes it.
- “Door load not available.” Provide a representative dummy, mass, and center of gravity when load affects alignment.
- “Golden sample controls everything.” Keep drawings and measurable limits as the engineering master.
- “All hardware with the same thread is equivalent.” Hinge, latch, insert, and fastener geometry can alter alignment.
- “Medical certified sheet metal enclosure.” Request the exact certification scope and record; panel alignment alone does not certify a finished device.
Frequently Asked Questions
What is a good panel gap for a medical equipment enclosure?
There is no universal value. The OEM should select a nominal gap from industrial design, movement clearance, coating, gasket, service access, enclosure scale, production capability, and risk. The drawing must also define tolerance, taper, flush offset, measurement points, and the inspection condition.
What is the difference between gap, flush, and flatness?
Gap is the distance between adjacent edges. Flush is the height step between adjacent surfaces. Flatness describes variation within one surface. They are related through the assembly stack but require separate acceptance criteria.
Should door gap be measured latched or unlatched?
The drawing or inspection plan should state the required condition. For a door whose normal closed state uses latches and a gasket, latched measurement is often relevant, but the OEM must define latch setting, gasket condition, torque, support plane, and installed load. Unlatched measurements may still be useful for diagnosing hinge or frame geometry.
Can powder coating make a compliant bare-metal gap fail?
Yes. Coating adds thickness at both edges, can build unevenly around geometry, and may affect hardware seating. Design for the specified finish and make final acceptance on the finished mechanical assembly.
Does stainless steel automatically improve gap and flush?
No. Material choice does not replace datum design, forming control, welding strategy, locating features, hinge and latch control, or final inspection. Brushed stainless also adds grain-direction and surface-reflection requirements that can amplify visible misalignment.
How should flushness be measured?
Suitable methods may include a straightedge with feeler gauges, a step gauge, depth gauge, indicator fixture, or approved digital method. The correct tool depends on tolerance and geometry. Define datum support, contact locations, measurement points, surface condition, and reporting rules.
Can a photograph prove gap-and-flush compliance?
A photograph can document overall appearance and seam continuity, but perspective and lighting make it unsuitable as the only dimensional evidence. Pair controlled photographs with recorded gauge results.
Should every visible seam have the same tolerance?
Not necessarily. Classify seams by user visibility, functional movement, cleanability, service, and product architecture. Apply tighter requirements where they add customer or functional value, and practical requirements elsewhere.
What should MSTFAB receive for a gap-and-flush DFM review?
Send the complete STEP assembly, matching dimensioned drawings, seam and surface map, nominal gaps, flush limits, measurement locations, hinge and latch details, gasket, material and finish, representative door loads, support condition, target quantity, and first-article requirements.
Does MSTFAB manufacture complete medical equipment?
No. MSTFAB manufactures custom unpopulated sheet metal enclosure shells and mechanical parts from buyer drawings. We do not supply the finished medical device, electronics, software, clinical functions, medical validation, or final product certification.
Who approves the final gap-and-flush requirement?
The OEM’s responsible engineering, industrial design, quality, and where applicable regulatory teams approve the product requirement. MSTFAB can provide DFM feedback and manufacturing evidence, but buyer approval is required for design changes and final acceptance criteria.
When should a gap-and-flush FAI be repeated?
Repeat or extend the review when a change can affect the seam: material, thickness, tooling, welding fixture, hinge, latch, gasket, door load, locating feature, finish route, inspection fixture, assembly sequence, or packaging. The exact revalidation scope should follow the buyer’s risk and quality agreement.
Conclusion: Specify the Seam, Not the Adjective
A reliable medical enclosure drawing does not ask for “perfect alignment.” It identifies the important seam, gives it a nominal gap and flush limit, defines where and how to measure it, states the finished assembly condition, and assigns responsibility for approval. That turns appearance from a late argument into a controlled engineering input.
MSTFAB can manufacture the unpopulated sheet metal shell, control approved datums and processes, inspect finished gap-and-flush CTQs, document the first article, and protect the assembly for export. The medical equipment OEM retains responsibility for the complete product, installed loads, intended use, regulatory requirements, validation, and final release.
Good seams are rarely accidental. They are the quiet result of useful datums, realistic tolerances, controlled hardware, a sensible fixture, finished-condition inspection, and several people agreeing what “good” means before the first laser-cut blank appears.
Written by: MSTFAB Sheet Metal Engineering Team
Technical review: Fabrication and Quality Team
Last reviewed: August 2026
 WeChat Contact
 WhatsApp Me Directly