Medical enclosure external hardware DFM defines how hinges, latches, handles and visible fasteners meet the sheet metal shell without creating unreachable gaps, awkward wipe paths, weak mounting zones or surprise coating interference.
The OEM must define the intended cleaning or disinfection method and validate the finished device. MSTFAB translates buyer-approved requirements into manufacturable panel geometry, cutouts, reinforcements, fastener interfaces, finish masks and measurable first-article checks.
Scope: MSTFAB supplies empty custom sheet metal enclosure shells and mechanical parts. We do not supply electronics, wiring, clinical functions, cleaning validation, sterilization claims or finished medical devices.
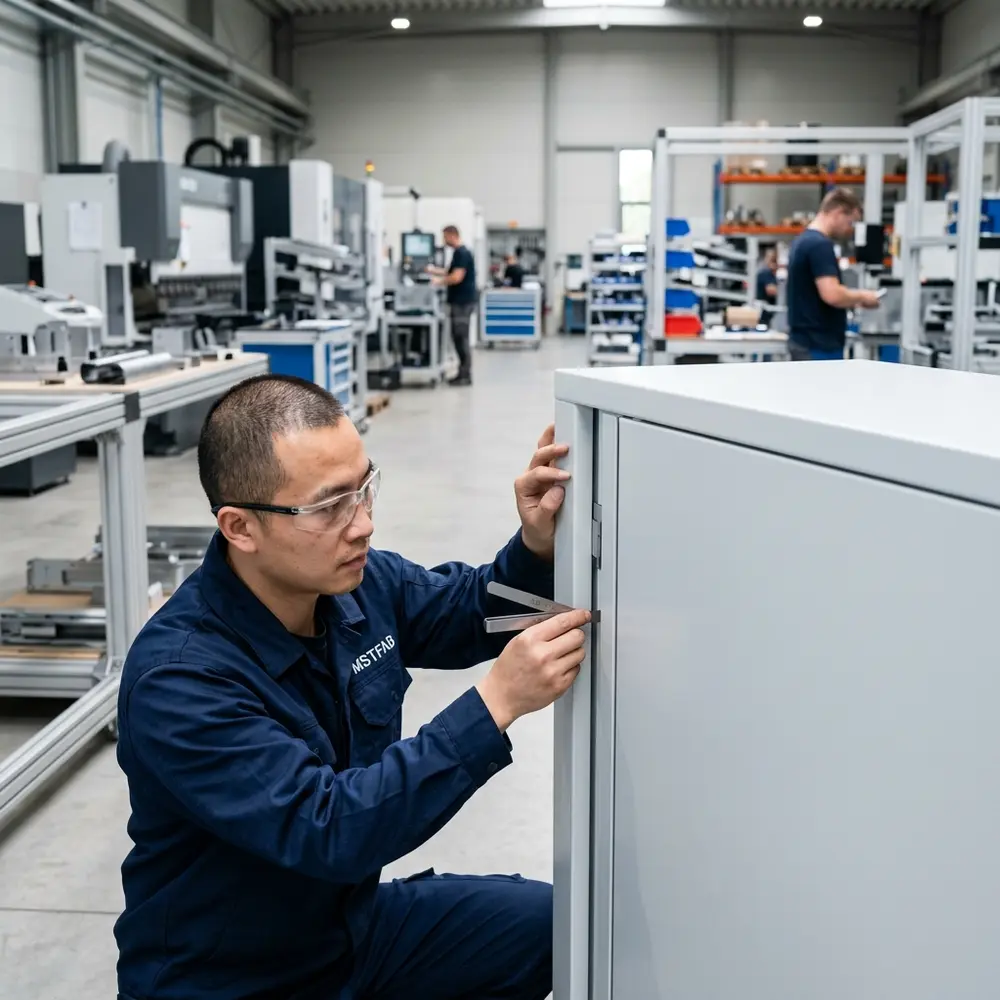
Why this page now focuses on external hardware
MSTFAB already publishes a broader medical enclosure cleanability and cosmetic-finish checklist. Keeping two pages aimed at the same search question would make Google choose between siblings at the dinner table. Nobody enjoys that, least of all the website.
This guide therefore owns a narrower engineering decision: the mechanical interface around external hinges, latches, handles and fasteners. Material selection, general cosmetic classes and the full exterior checklist remain covered in our medical enclosure cleanability and cosmetic finish checklist.
The narrower scope is also more useful to a buyer. A note saying “easy to clean” cannot be inspected. A drawing that identifies a 20 mm wipe lane around a latch, a concealed hinge keep-out zone and an approved fastener head can.
Begin with the OEM cleaning requirement, not a hardware catalogue
The same enclosure can live in a dry laboratory, a mobile treatment cart or a room with frequent disinfectant wipe-down. Those environments may require different materials, finishes and hardware exposure. The RFQ should state the intended use environment, approved cleaning agents if known, expected frequency, wet-contact zones and whether the surface is merely wiped or forms part of a validated reprocessing process.
FDA guidance on reusable medical-device reprocessing places formulation and scientific validation of reprocessing instructions with the device manufacturer. That is an important responsibility boundary: MSTFAB can manufacture geometry to the approved design, but a sheet metal supplier cannot validate a finished device’s cleaning instructions by looking at a CAD screenshot. The official FDA reprocessing guidance provides the regulatory context.
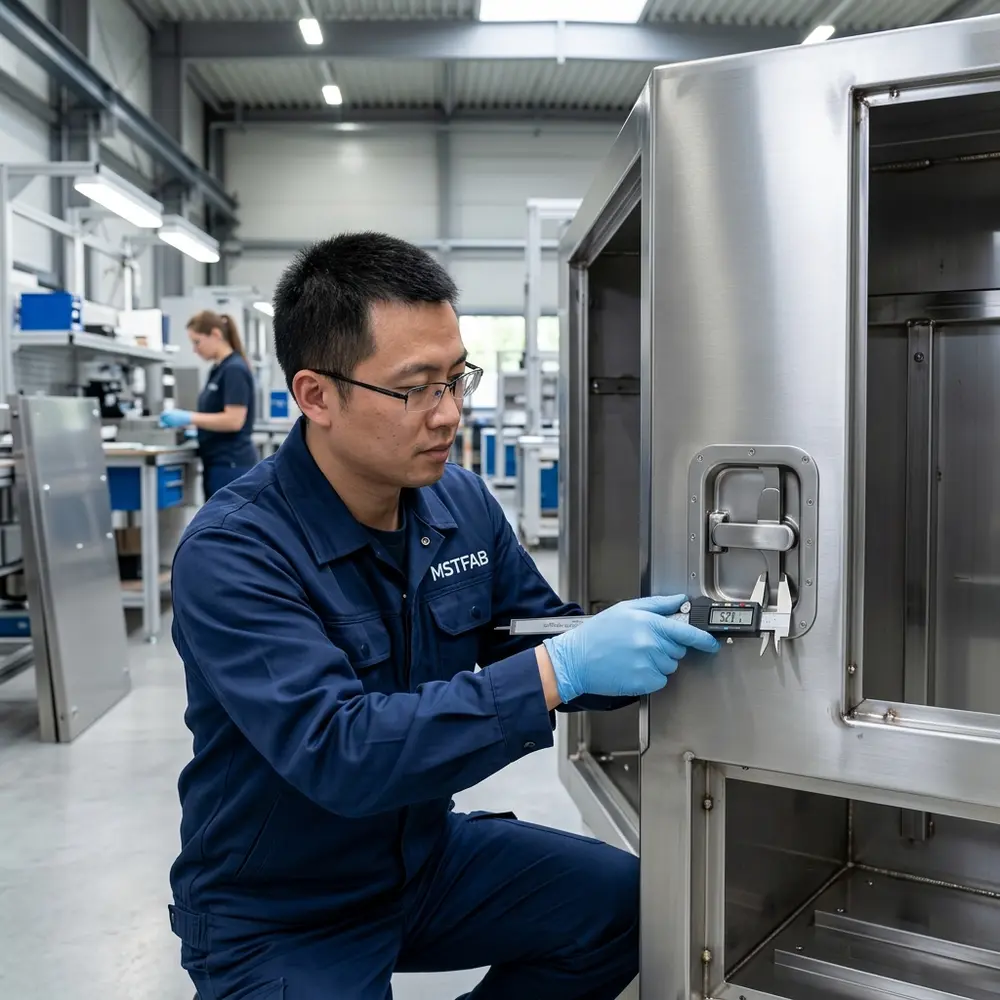
Translate the requirement into hardware-zone drawings
Do not leave external hardware location only in the 3D model. The controlled 2D drawing should identify the hardware part number or approved equivalent, cutout, mounting-hole pattern, orientation, panel thickness, finish condition, masking, visible-surface class and critical clearances.
For each external hardware zone, define what the buyer actually cares about:
- Minimum reachable surface around the hardware
- Permitted gap, projection or recess
- Door swing and service-tool clearance
- Drain direction for any pocket or horizontal surface
- Finished-panel dimensions after coating
- Acceptable fastener head and visible orientation
- Inspection condition with the specified hardware installed
These are interface requirements. They cannot be solved by asking the sheet metal shop to “use its standard latch,” because the standard latch has never met your nurse, technician, detergent or service manual.
Hinges: choose the tradeoff before freezing the door
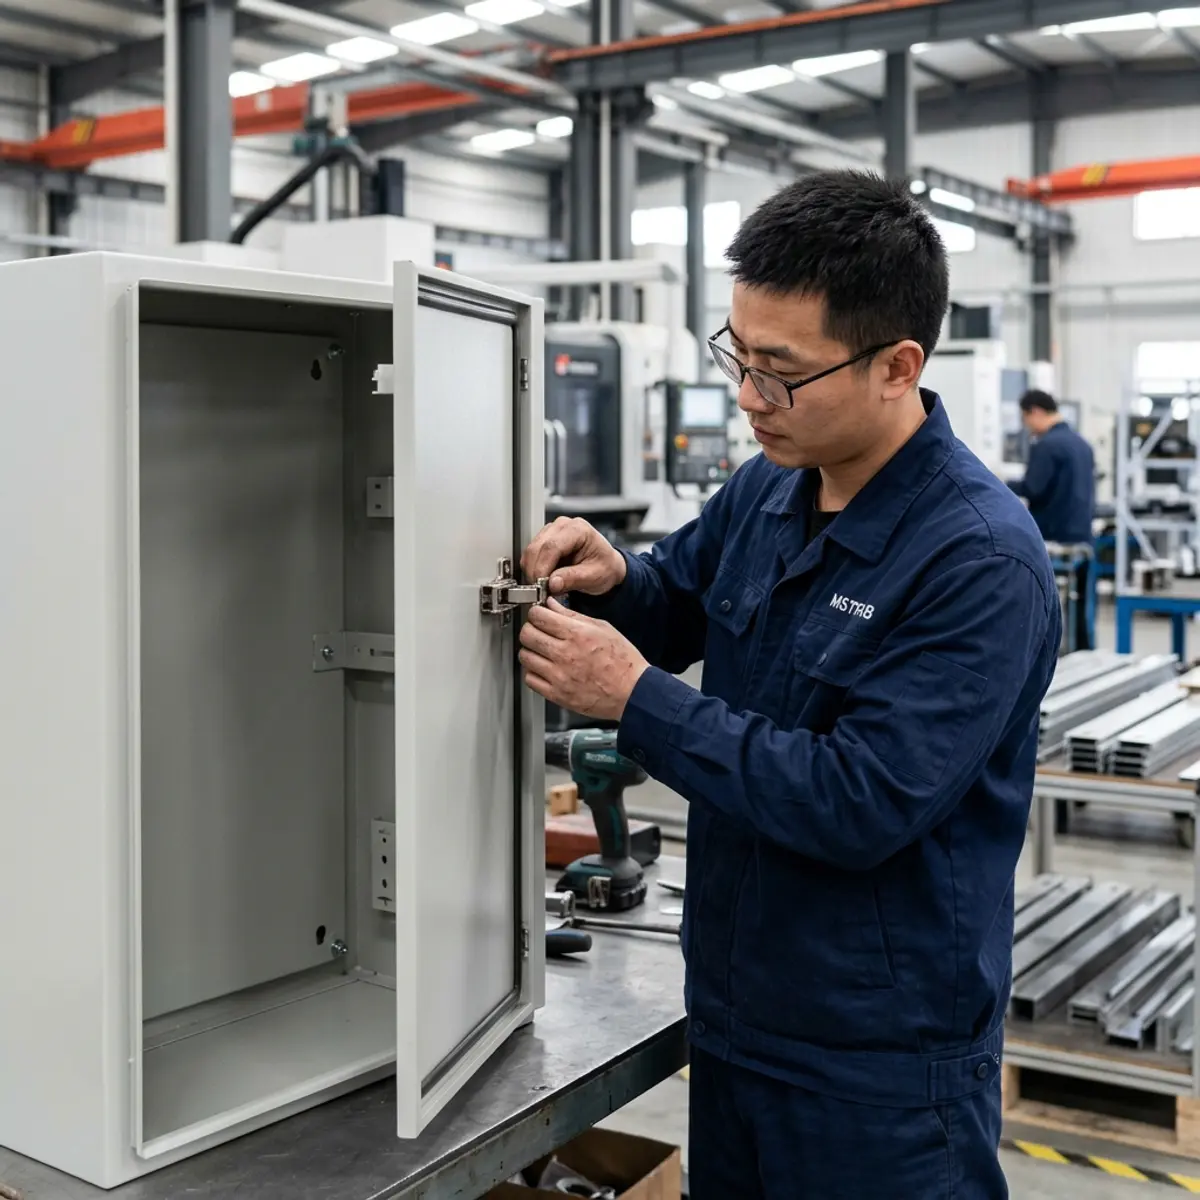
An external hinge is simple to see, install and service, but its leaves, knuckles, pin and mounting fasteners add surface geometry. A concealed hinge can leave the exterior cleaner, yet it consumes internal space and may complicate door returns, gasket compression, opening angle and installation access.
Neither option is automatically more “medical.” Select it from the actual cleaning, service and structural needs. During DFM, review hinge position, hardware access, bend sequence, backing or reinforcement, weld distortion, coating allowance, door removal and the gap between hinge, door and frame.
Do not create the almost-cleanable gap
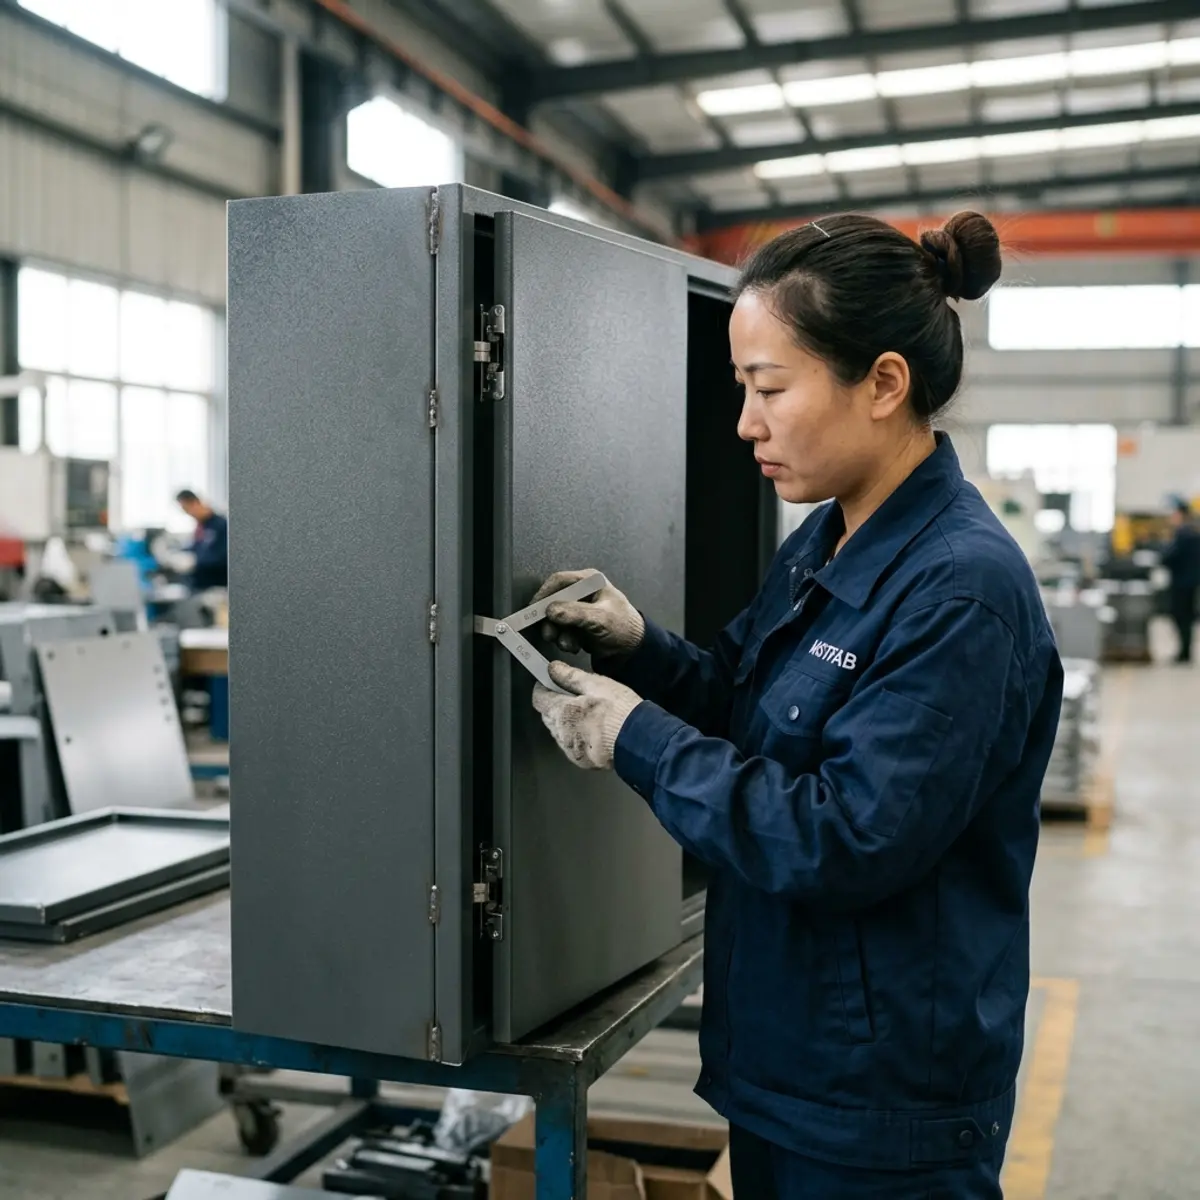
A wide accessible gap can be intentionally cleaned. A fully closed and properly sealed interface follows a different strategy. The frustrating option is the arbitrary narrow gap that accepts residue but rejects every practical wipe or tool.
Specify the intended condition instead of copying a number from another cabinet. Hinge geometry, door load, coating thickness, gasket compression and assembly variation all influence the finished gap. Functional and wipe-access checks should use the real hardware, not an optimistic rectangle in CAD.
Latches: access, compression and panel stiffness are one problem
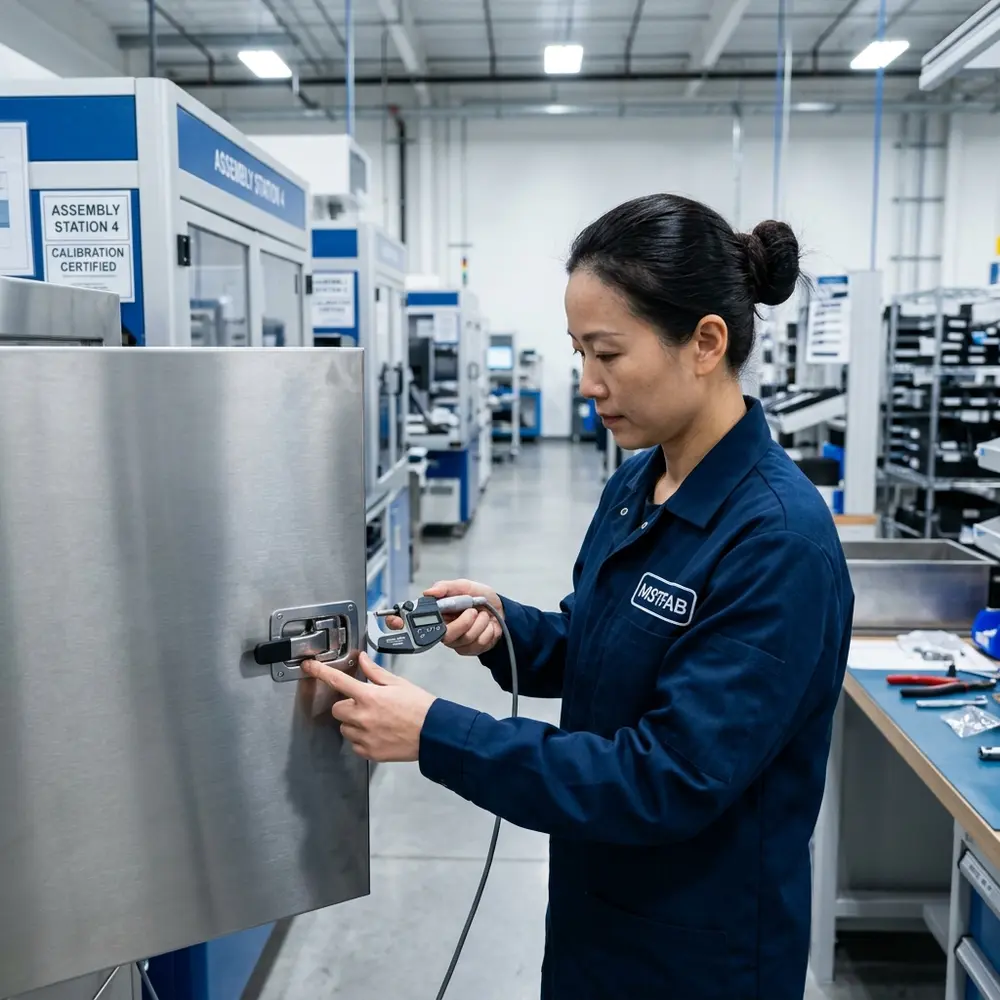
Quarter-turn, compression, swing-handle and multi-point latches create different cutouts and load paths. A flush latch may reduce projection, but its recess can become a pocket. A compression latch may support gasket performance, but it also pulls on a local area of thin sheet.
Review latch cutout corner radii, anti-rotation features, edge distance, local reinforcement, cam clearance, grip range, coating buildup and access for installation. If the latch pulls the panel into a visible dish, the hardware may function while the enclosure looks as if it is apologizing.
The drawing should define the finished door relationship: closed gap, flushness, pull-in, handle orientation and acceptable local distortion. For a pocket, define whether liquid can collect and whether every surface can be reached under the buyer’s cleaning method.
Handles: make room for hands, cloths and structure
A handle needs finger clearance and a load path. It may also need enough surrounding access for routine wiping. Define mounting-hole spacing, orientation, minimum hand clearance, visible fastener side, backing plate or formed reinforcement, and the surface condition beneath the handle.
For welded or internally fastened handles, consider heat distortion and access before surrounding bends close the panel. For removable handles, specify whether washers, spacers or sealing features are part of the buyer-controlled assembly. MSTFAB should not quietly substitute handle hardware because the holes happen to line up.
Visible fasteners: every head needs a reason
External screws may be necessary for service access. The goal is not a heroic campaign against all visible hardware; it is a controlled strategy. Decide whether the fastener is removable, captive, flush, sealed, tamper-resistant or installed from the clean side.
Countersinking thin sheet requires review. A deep countersink can remove too much material, distort the hole or leave the head proud after coating. A press-in fastener depends on correct hole size, material hardness, edge distance and installation direction. Weld studs avoid an external head but bring weld marks, distortion and finish preparation.
Hems, overlaps and weld transitions around hardware
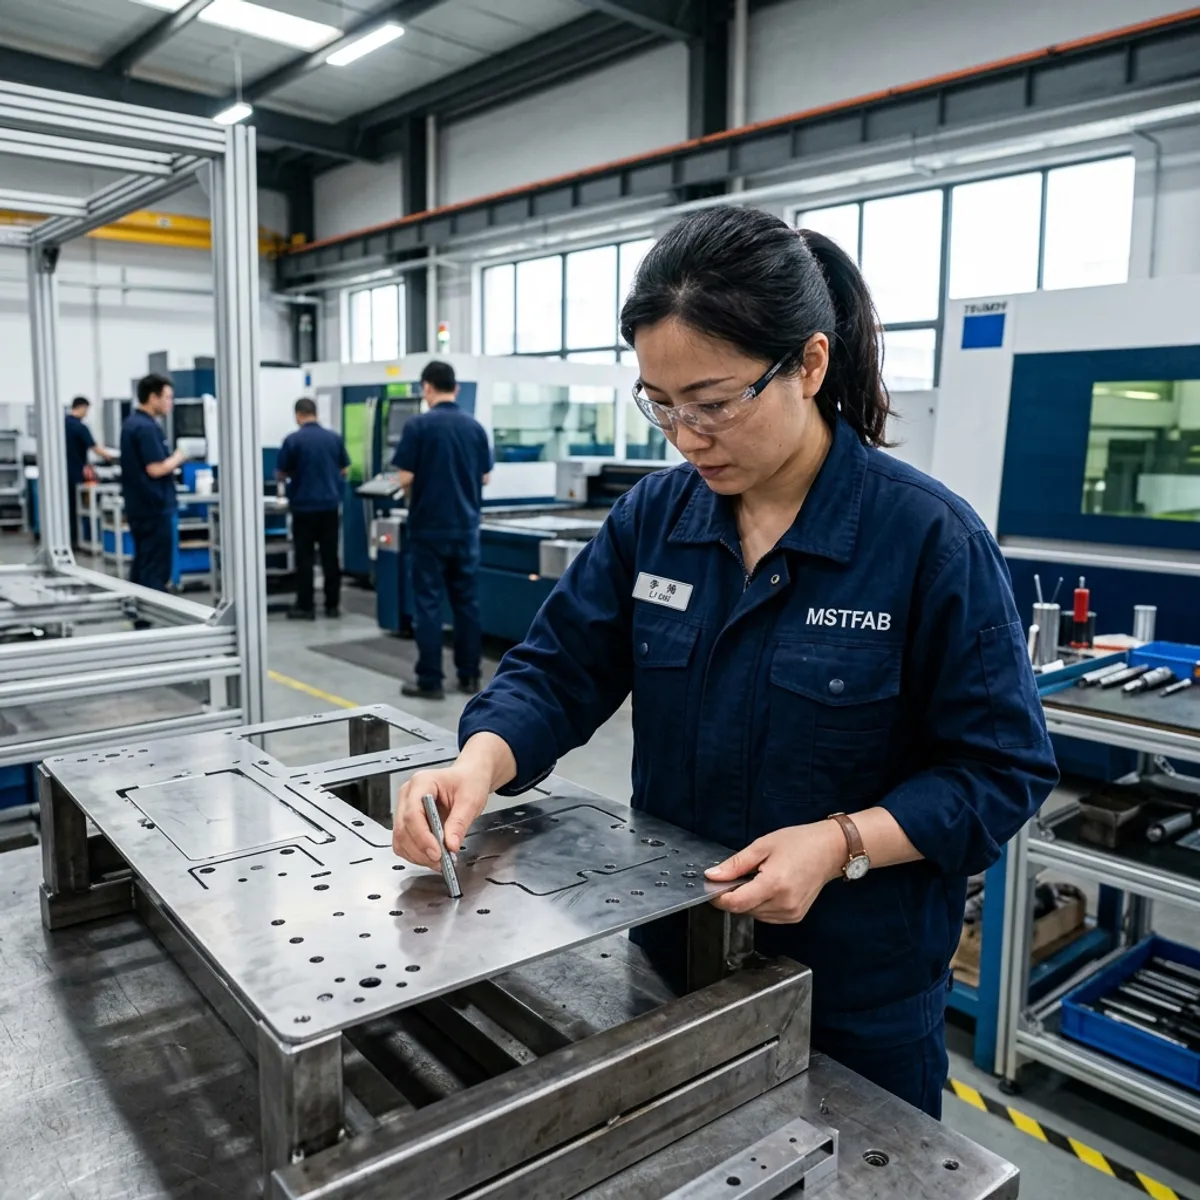
Hemmed edges can remove an exposed raw edge and increase stiffness, but the fold creates an interface that must match the cleaning strategy. Open hems, closed hems and sealed edges behave differently. The drawing should define the intended edge rather than asking the supplier to make it “smooth.”
Overlapping panels can simplify assembly yet create a ledge or capillary gap. Around external hardware, check whether the overlap blocks wipe access, traps liquid or shifts the hardware mounting plane. Welded transitions may be blended for appearance and accessibility where specified, but grinding also changes material thickness and surface texture. Cosmetic blending and structural weld acceptance are related, not identical.
Finish allowance belongs in the hardware stack
Powder coating changes hole size, edge thickness and fit. Brushed stainless finishes introduce grain direction and cosmetic consistency. Passivation, when specified for stainless steel, is a process requirement rather than a magic eraser for poor geometry.
Define masks for threads, grounding contact zones, bearing surfaces and close-fitting hardware. Confirm whether the latch or hinge is installed before or after finishing. If suppliers quote the bare-metal cutout while the hardware arrives after coating, the assembly team may discover that paint also believes in tight tolerances.
First-article checks should reproduce the real interface
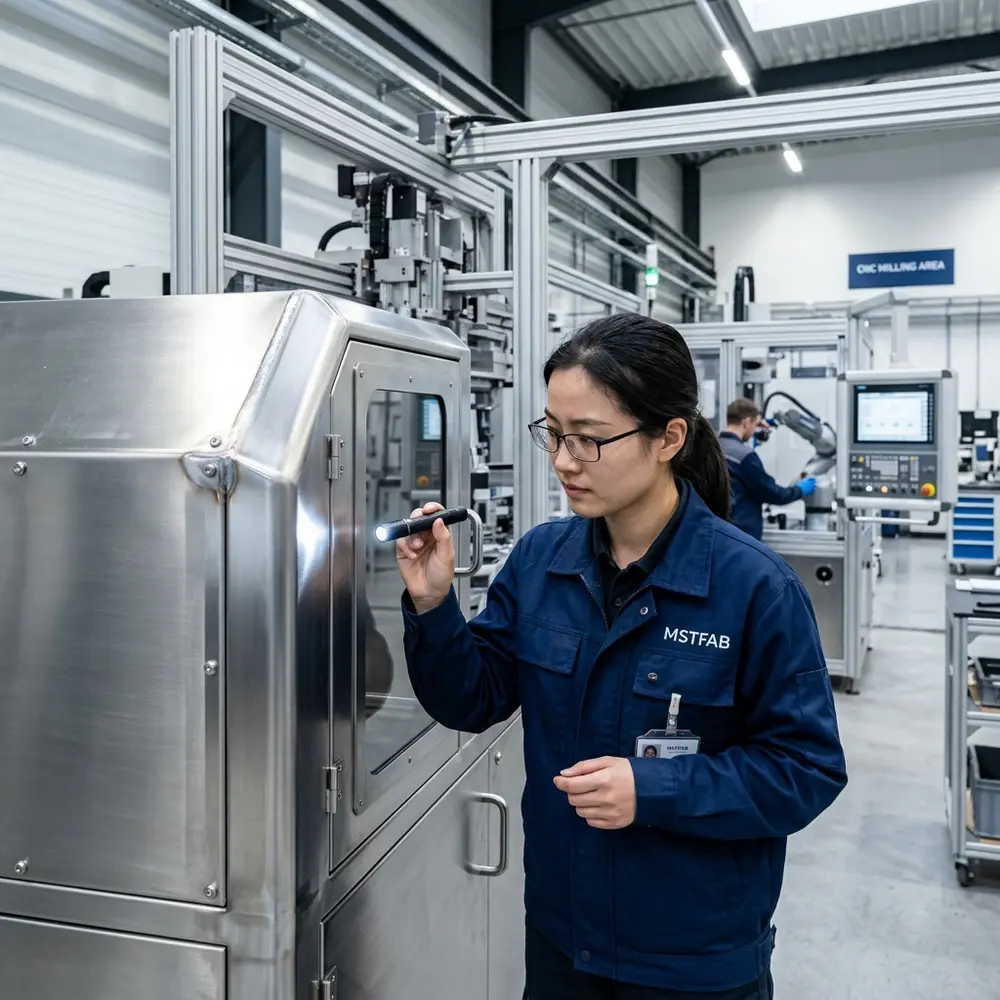
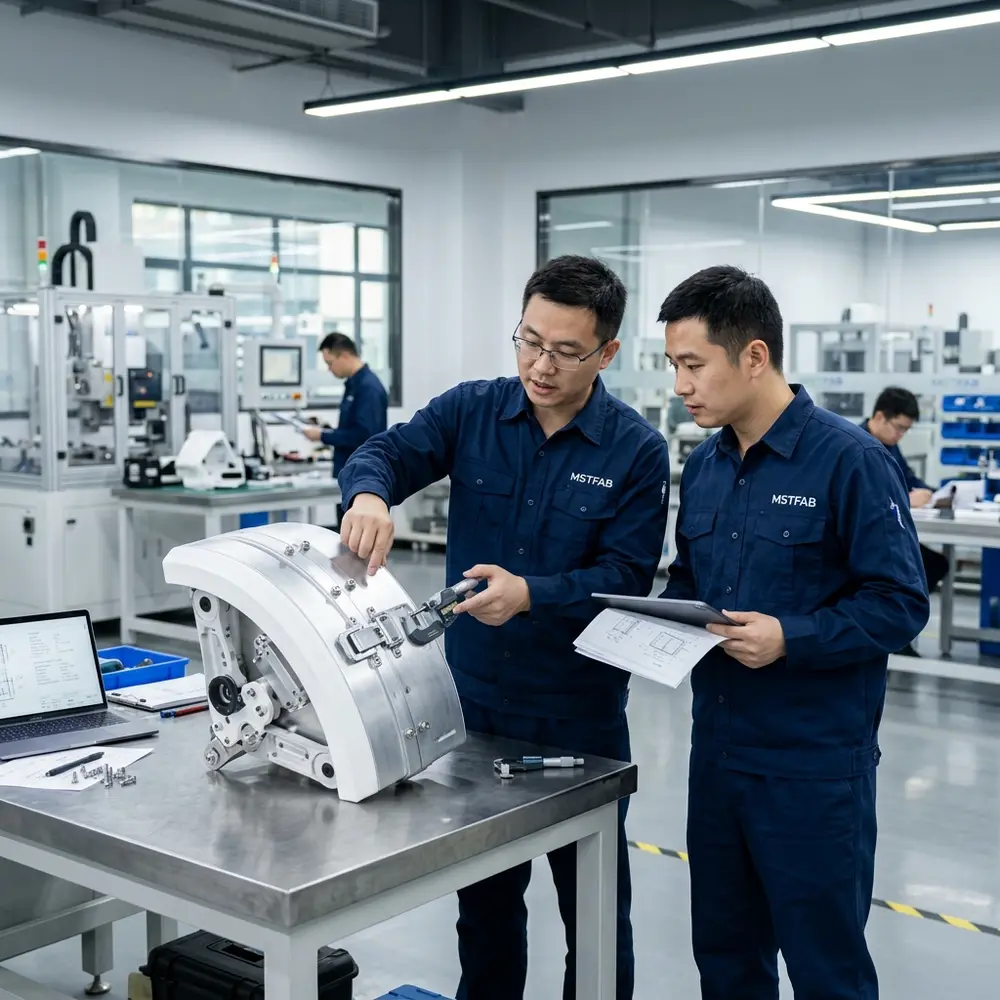
A first article should use the approved hinge, latch, handle and visible fasteners whenever practical. A cutout-only report cannot confirm swing, pull-in, wipe access, local flatness or tool clearance.
| Hardware zone | First-article evidence | Buyer question answered |
|---|---|---|
| Hinge | Door swing, removal, hinge-side gap, fastener access and coating clearance | Can it open, be serviced and be reached as intended? |
| Latch | Cutout fit, pull-in, closed gap, local flatness, cam clearance and orientation | Does it close correctly without distorting the door? |
| Handle | Hand clearance, mounting strength, backing, orientation and surrounding access | Can users grip and clean around it safely? |
| Visible fastener | Head condition, seating, thread check, coating allowance and approved appearance | Is the installed condition functional and cosmetically acceptable? |
Responsibility split: keep the evidence honest
OEM or device manufacturer
- Defines intended use and cleaning exposure
- Selects and approves hardware
- Owns device risk management and validation
- Approves finished-device labeling and compliance
MSTFAB build-to-print scope
- Reviews manufacturability of shell and interfaces
- Controls cutouts, bends, welds and finish masks
- Installs specified mechanical hardware when quoted
- Inspects agreed dimensions, fit and appearance
RFQ checklist for external hardware zones
- STEP model and controlled 2D drawing with revision
- Hardware manufacturer, part number and approved alternatives
- Material, thickness and surface finish
- Cleaning exposure supplied by the OEM
- Minimum wipe-access or service clearances
- Door swing, removal and tool-access requirements
- Finished gap, flushness and latch pull-in criteria
- Visible fastener head, orientation and cosmetic class
- Thread, bearing and contact-area masking
- First-article fit, photo or measurement records required
- Prototype, batch and annual quantities
- Packaging protection for finished cosmetic surfaces
FAQ
Can MSTFAB certify an enclosure as easy to clean?
No. MSTFAB can fabricate and inspect buyer-defined mechanical geometry. The OEM or finished-device manufacturer must define and validate the cleaning or reprocessing method and make any regulatory or performance claim.
Are concealed hinges always better for medical equipment?
No. They can reduce external hardware but may reduce internal clearance, opening angle or service access. The right choice depends on the approved use, cleaning, structural and maintenance requirements.
Can all visible screws be made flush?
Not automatically. Sheet thickness, fastener head, countersink depth, load, coating and service requirements must be reviewed. A flush appearance should not create a weak or distorted hole.
Does MSTFAB supply the hinge and latch?
When included in the quotation, MSTFAB can source or install buyer-specified mechanical hardware. The approved manufacturer, part number, equivalent policy and inspection condition should be stated before production.
What is the best prototype check?
Install the real hardware on a finished first article and review door motion, pull-in, gaps, local flatness, hand access, wipe access and tool clearance together. It is cheaper than explaining later why every individual dimension passed while the assembly did not.
Review your external hardware before release
Send MSTFAB the controlled drawings, hardware specifications, material, finish, quantities and buyer-defined interface requirements. We will review the sheet metal and mechanical fit-up risks before quotation.
 WeChat Contact
 WhatsApp Me Directly