
A telecom enclosure can pass every bare-metal dimensional check and still fail during final assembly. Powder can insulate a grounding pad, fill a threaded insert, tighten a removable gland plate, reduce latch engagement or leave a visible cabinet door with unacceptable texture. These are not only cosmetic defects. They are predictable interface problems that should be controlled before the finishing line.
Quick answer: A telecom enclosure powder-coating and masking plan should define the complete finish route, color and texture, target thickness, grounding masks, threaded-feature protection, PEM hardware sequence, DIN-rail and rack interfaces, door and latch clearances, gasket lands, removable gland plates, connector cutouts, tight mating surfaces, cosmetic zones and post-coating inspection. OEM buyers should freeze these requirements on controlled drawings before production and approve a finished first article, not only a bare-metal sample.
Scope note: MSTFAB manufactures drawing-based empty telecom enclosure shells, doors, rack structures, mounting plates, gland plates, brackets, grounding studs, installed hardware and specified surface finishes. We do not design the finished telecommunications system, select network electronics, establish the buyer’s bonding architecture or certify the complete equipment. The buyer or integrator owns electrical design, environmental requirements, component selection and final system validation.
What Must a Telecom Enclosure Finish Specification Define?
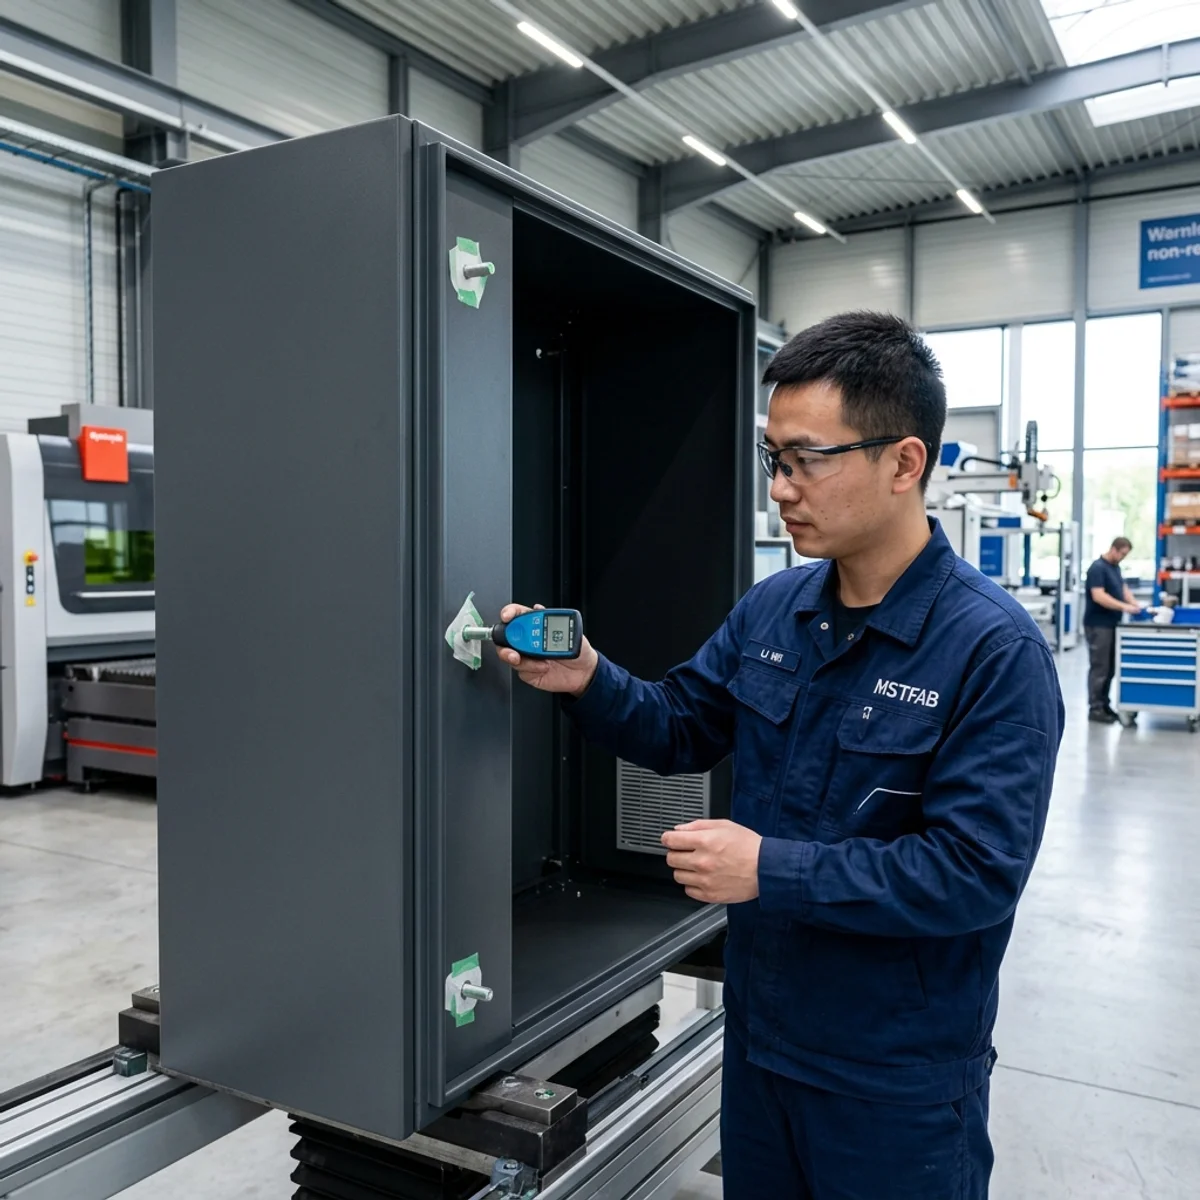
A note that says only “powder coat black” is not a complete manufacturing requirement. The supplier still needs to know the substrate preparation, coated surfaces, excluded surfaces, color reference, gloss or texture, acceptable thickness range, corrosion expectations, visual zones and inspection method. The drawing also needs a masking map tied to functional interfaces.
The finish route may differ for cold-rolled steel, galvanized steel, aluminum and stainless steel. Pretreatment, primers, powder chemistry and surface preparation should be selected for the project environment. The buyer should state performance requirements and approve any required samples or qualification evidence rather than assuming all black coatings behave the same.
| Buyer decision | Information to place on controlled documents | First-article evidence |
|---|---|---|
| Finish system | Substrate, pretreatment, primer where required and powder type | Process record or agreed supplier evidence |
| Appearance | Color reference, gloss or texture and approved sample | Comparison under defined lighting |
| Functional thickness | Target or acceptable range and measurement locations | Coating-thickness readings at agreed points |
| Masking | Exact zones, dimensions, sides and protected threads | Visual mask check and functional assembly test |
| Acceptance | Cosmetic classes, defects, sampling and packing protection | Finished inspection report and release sample |
Why Powder Coating Changes Functional Fit
Powder coating adds material to surfaces. When two coated faces approach each other, the total stack can include coating on both parts. A door return, hinge leaf, latch cam, rack bracket or gland plate that fits comfortably in bare metal may become tight after pretreatment and curing. Edge geometry and Faraday-cage effects can also make thickness less uniform than a simple nominal value suggests.
Heat exposure during curing can reveal distortion in large thin panels or welded doors. Hanging and contact points can leave marks. Masking edges can create ridges. Rework may damage corrosion protection or appearance. A useful DFM review therefore combines geometry, finishing, assembly sequence and inspection rather than treating coating as a decorative purchase-order line.
The critical approval condition is the finished assembly. Bare-metal fit checks remain valuable, but they do not prove ground continuity, final latch feel, gasket compression, connector clearance or cosmetic acceptance.
Common Masking Methods and Their Uses
Masking should be selected according to feature geometry, cure temperature, required edge quality and production volume. The table below gives practical examples; the finishing supplier should confirm process compatibility for the approved coating route.
| Masking method | Typical use | DFM and inspection points |
|---|---|---|
| High-temperature tape or die-cut masks | Ground pads, gasket lands and defined flat zones | Control dimensions, edge position, adhesion and clean removal. |
| Silicone plugs and caps | Threaded holes, studs, pins and tube ends | Match feature size, cure temperature and required depth. |
| Temporary screws or sacrificial hardware | Selected threaded features where approved | Define removal, debris control and risk to first threads. |
| Reusable custom masks or fixtures | Repeat production with complex zones | Validate location, wear, cleaning and traceable setup. |
The 12-Detail Powder Coating and Masking DFM Checklist
1. Freeze the Complete Finish Route
Identify the substrate and every required preparation step. State whether internal surfaces, hidden returns, welded frames, removable panels and hardware receive the same coating. Define color with a recognized reference such as an approved RAL value where applicable, but also state gloss or texture because the same color can look different across powder systems.
If outdoor corrosion performance is important, provide the environmental and qualification requirements. Avoid substituting a vague marketing term such as “weatherproof” for a controlled coating specification. MSTFAB’s surface treatment guide provides an overview of common sheet metal finishing routes.
- Put on the drawing: substrate, pretreatment, coating system, color, texture and coated surfaces.
- Ask for evidence: approved finish sample and project-specific process confirmation.
- Red flag: the RFQ specifies only a color name.
2. Define Grounding and Bonding Masks
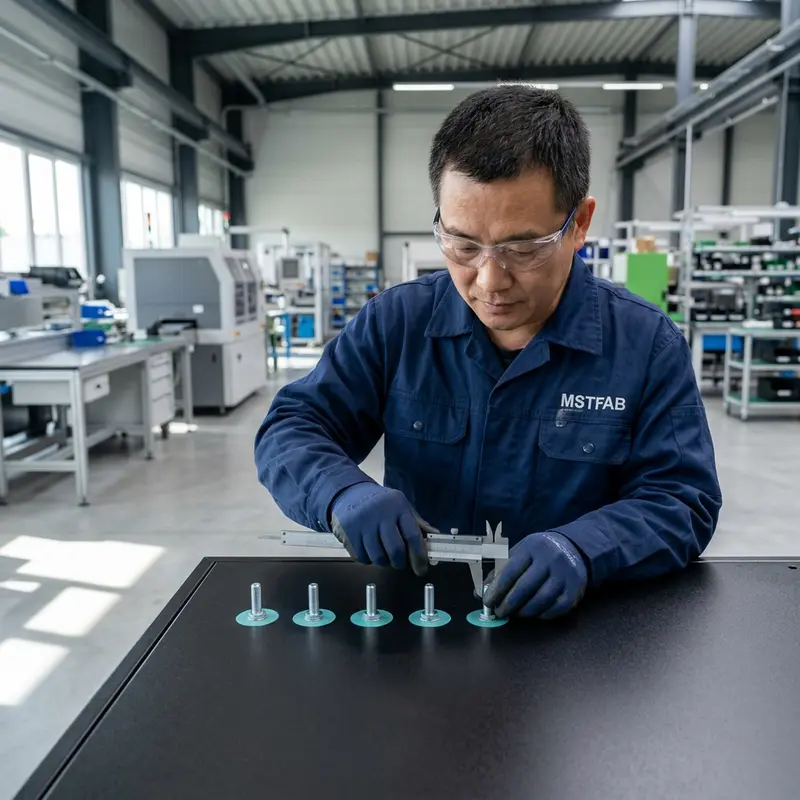
Powder coating is electrically insulating. Every location requiring metal-to-metal contact should be identified by the OEM’s electrical design and converted into a measurable mask. Define the pad shape, diameter or boundary, the side of the panel, nearby thread protection and whether a conductive stud or serrated hardware is part of the approved interface.
A note such as “ensure grounding” is not enough for production. The coating operator needs geometry. The final system owner should validate continuity after assembly because a visually bare pad alone does not prove the complete bonding path.
- Put on the drawing: exact mask geometry, datum location, surface side and related hardware.
- Ask for evidence: visual mask inspection and buyer-defined continuity verification.
- Red flag: grounding zones are selected by the coating operator without an electrical drawing.
3. Protect Threaded Holes, Studs and Inserts
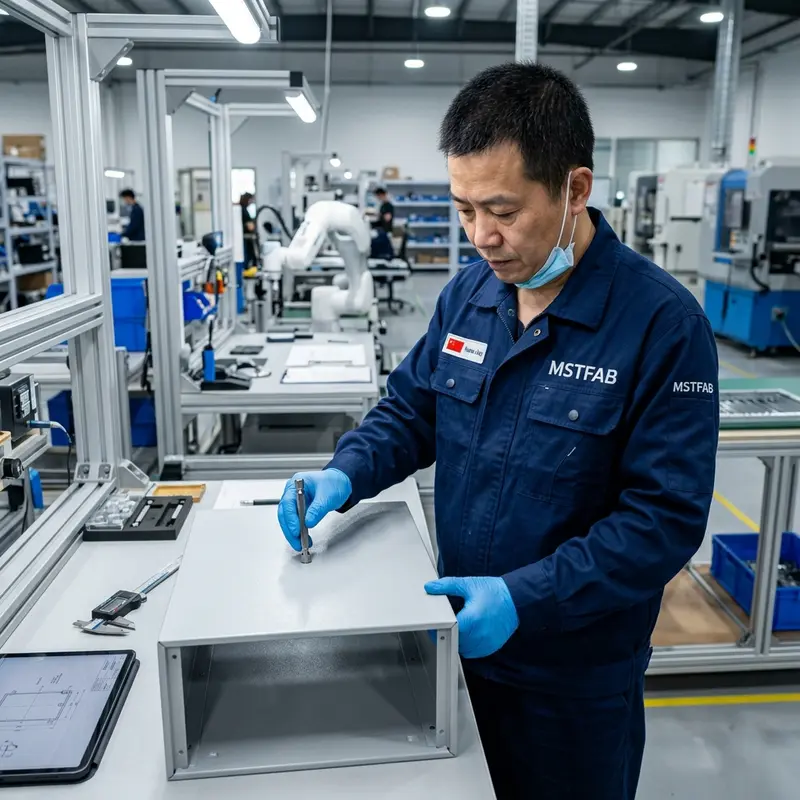
Powder in threads can increase installation torque, reduce usable engagement and cause cross-threading. Identify every feature that must accept hardware after finishing, including welded studs, tapped holes, nuts, rivet nuts and blind inserts. Define whether the complete depth or only an entry region needs protection.
Post-coating thread chasing may be appropriate only when explicitly approved. It adds labor, creates debris and can remove protective finish around the feature. A repeatable plug or cap is usually easier to inspect than uncontrolled rework after coating.
- Put on the drawing: protected thread list, mask depth and acceptable verification method.
- Ask for evidence: thread gauge or representative-fastener check after coating.
- Red flag: all threads are expected to be cleaned manually after the batch is coated.
4. Decide the PEM Hardware Installation Sequence
Some self-clinching hardware is installed before coating; other project hardware may be installed afterward. The sequence affects electrical contact, coating coverage, thread protection, visual appearance and press access. Define which inserts, studs and nuts are present during finishing and which are installed into the finished part.
When hardware is installed before coating, review masking and powder buildup around the head or shank. When installed afterward, confirm the coating will not crack or prevent the required seating. The approved sequence should be reflected in the drawing and routing.
- Put on the drawing: hardware part number, installation stage and masking requirement.
- Ask for evidence: finished hardware seating and thread checks.
- Red flag: the BOM lists hardware but does not define whether it is coated in place.
5. Check DIN-Rail and 19-Inch Rack Interfaces
DIN-rail brackets, rack rails, cage-nut openings and sliding support parts can be sensitive to coating buildup. Identify the datums and clearances that control equipment mounting. Decide whether specific contact faces or square-hole regions remain uncoated, receive a different finish or simply need additional design clearance.
For movable rails and adjustable brackets, verify the full intended range after finishing. Coating should not force installers to scrape surfaces, enlarge holes or hammer parts into position. Those actions reduce repeatability and may expose bare metal outside controlled zones.
- Put on the drawing: functional rail datums, hardware interfaces and finished clearance requirements.
- Ask for evidence: representative rack hardware or bracket fit on the first article.
- Red flag: only bare-metal rail spacing is approved.
6. Validate Door, Hinge and Latch Clearances
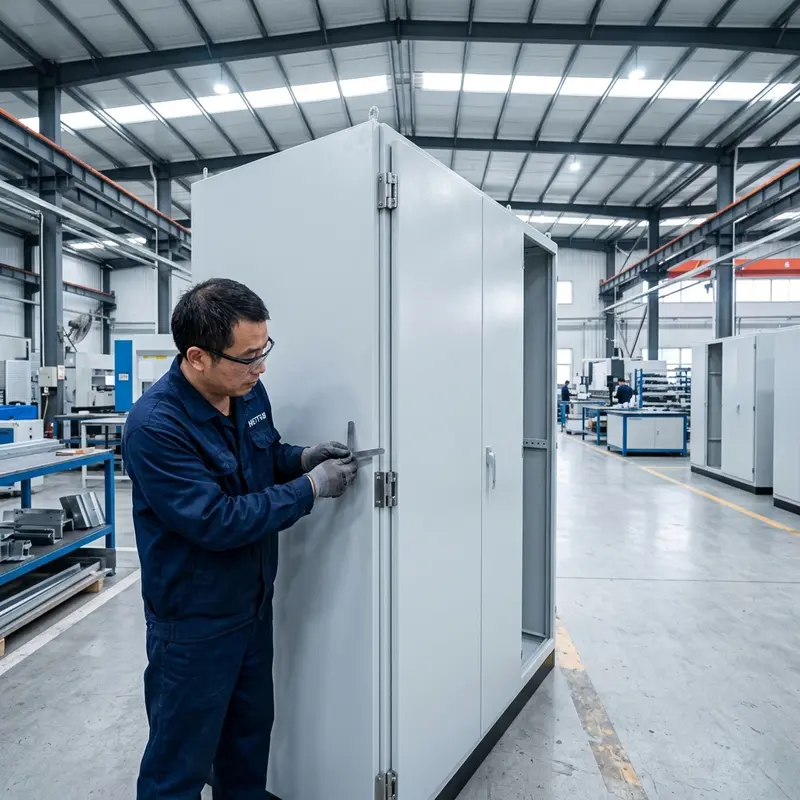
Door operation depends on multiple coated interfaces: hinge leaves, pins, returns, frame openings, latch cams and gasket compression surfaces. Check the door gap and operating sequence in the finished condition. A latch that closes only with excessive force can distort the door or create inconsistent gasket compression.
Large telecom doors may also move during curing or handling. Define the measurement state and acceptable gap where fit is critical. Include removable hinge pins, earth-bond leads and door-mounted hardware in the assembly review.
- Put on the drawing: finished door gaps, hinge treatment, latch engagement and operating condition.
- Ask for evidence: door-cycle and latch check on the finished first article.
- Red flag: bare-metal door operation is treated as final approval.
7. Define Gasket Lands and Sealing Surfaces
Gasket contact areas need a finish condition compatible with the buyer’s sealing design. Some projects require a continuous coated land; others define masked zones or controlled texture. The OEM should specify the gasket material, compression concept, surface requirement and any adhesion zone for applied foam or tape gaskets.
A poorly located masking edge can cross the sealing path and create a step. Overspray, hooks, weld spatter or coating defects on the land can also prevent consistent contact. Inspect the complete perimeter under suitable lighting before gasket installation.
- Put on the drawing: gasket path, finish or mask condition, joint limits and inspection zone.
- Ask for evidence: continuous visual inspection and representative gasket fit.
- Red flag: the sealing land is not identified until after coating.
8. Allow Finished Clearance for Removable Gland Plates
Gland plates often have coating on the plate edge and the surrounding cabinet opening. The combined buildup can turn a removable interface into a press fit. Include coating allowance in the design and verify plate insertion, fastener access, gasket position and removal direction after finishing.
Where electrical bonding is required, define the conductive interface separately from the sealing interface. Do not assume a fastener will automatically cut through coating and create a reliable path. The buyer should approve the bonding method.
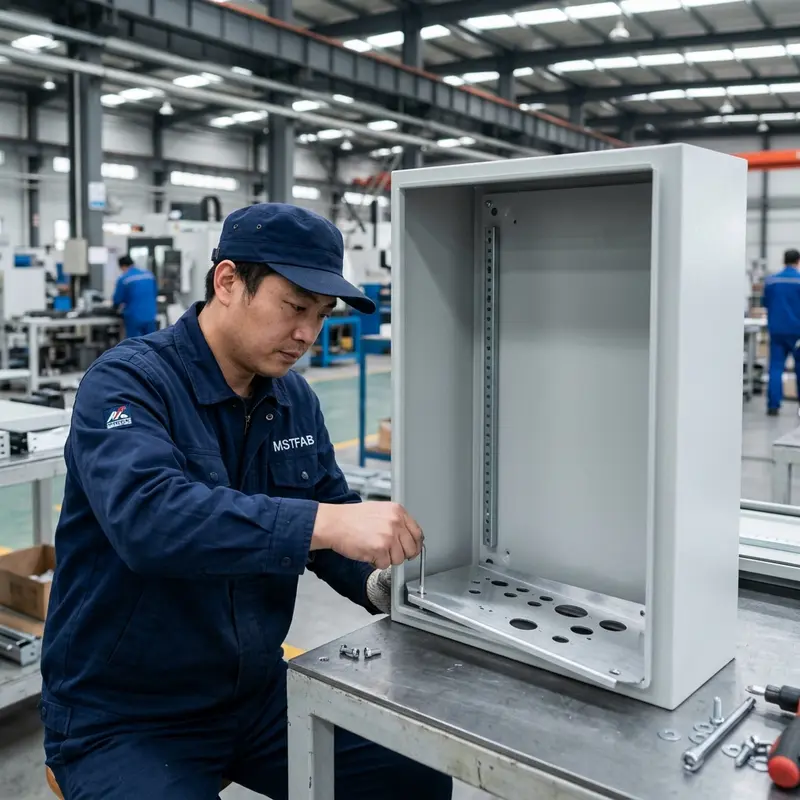
- Put on the drawing: finished fit, gasket, bonding zone, fasteners and removal direction.
- Ask for evidence: installation and removal demonstration after coating.
- Red flag: the plate is approved separately from the coated cabinet opening.
9. Protect Connector, HMI and Cooling Cutouts
Connector apertures, touchscreen openings, fan cutouts and heat-exchanger interfaces often use tight component or gasket fits. Define whether edges are coated, masked or mechanically finished, and include the resulting condition in the cutout tolerance. Check corner radii, edge buildup and nearby stud masks.
Use representative components, checking fixtures or controlled dummy interfaces for first-article approval. The sheet metal supplier can verify the contracted geometry; the buyer remains responsible for component selection, sealing and final equipment performance.
- Put on the drawing: finished cutout dimensions, edge condition and component interface.
- Ask for evidence: post-coating dimensional report or representative fit check.
- Red flag: the nominal cutout equals the component body with no finish allowance.
10. Review Tight Mating and Sliding Surfaces
Any tab, slot, telescoping member, removable panel or alignment feature with coating on both sides needs stack-up review. Reserve tight tolerances for interfaces that need them and provide sensible clearance elsewhere. This improves manufacturability without reducing functional control.
Masking every mating surface is not automatically the best answer. Bare zones may require corrosion protection or create visible boundaries. Compare adjusted geometry, selective masking and alternative finish sequences before release.
- Put on the drawing: finished clearance and which surfaces receive coating.
- Ask for evidence: complete movement or assembly check in the finished condition.
- Red flag: a tight bare-metal fit is expected to remain unchanged after both faces are coated.
11. Classify Cosmetic Surfaces and Defects
Visible doors and exterior panels usually need a different appearance standard from hidden brackets or internal supports. Define cosmetic classes, viewing distance, lighting, allowed touch-up, color and texture comparison, edge expectations and the defects that require rejection. This focuses inspection effort where the customer can see it.
Do not use subjective phrases such as “perfect finish” without an acceptance method. The guide to powder-coating cosmetic acceptance standards explains how buyers can divide visible zones and document evaluation conditions.
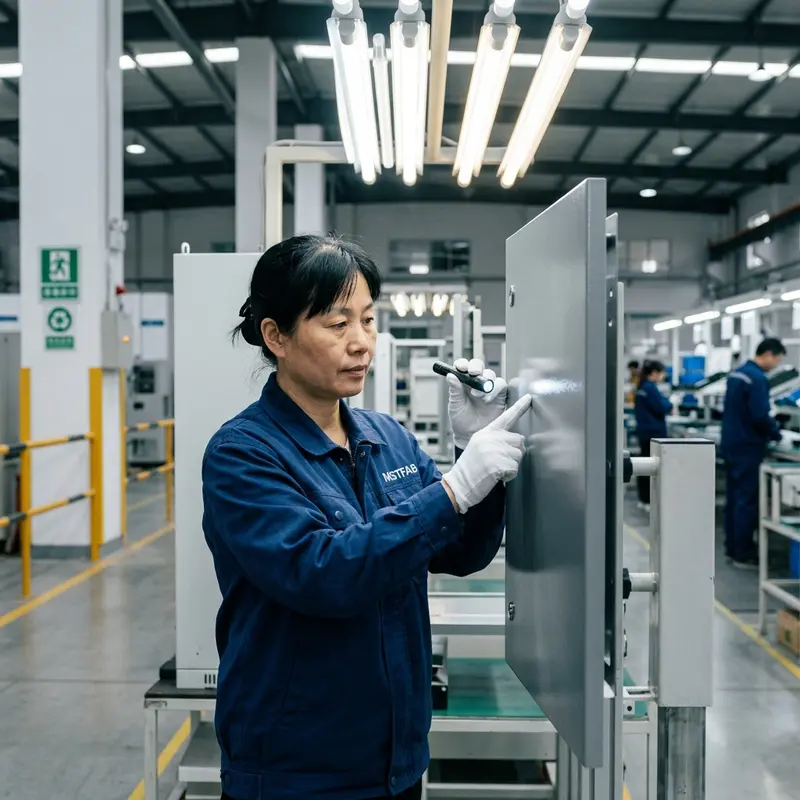
- Put on the quality plan: surface classes, viewing method, color sample and defect limits.
- Ask for evidence: first-article appearance approval and production sampling record.
- Red flag: hidden brackets and customer-facing doors carry the same undefined standard.
12. Inspect, Handle and Pack the Finished Enclosure
Finishing is complete only when usable parts reach the customer. Verify coating thickness at agreed locations, mask removal, thread condition, ground pads, door operation, gland plate fit and cosmetic surfaces before packing. Remove masking residue and loose debris without damaging the finish.
Protect doors, corners and Class A faces with non-abrasive separators, film, foam and project-appropriate export packaging. Prevent hardware bags, rails and loose panels from rubbing against coated surfaces. Packing supports should not concentrate load on thin doors or distort the cabinet.
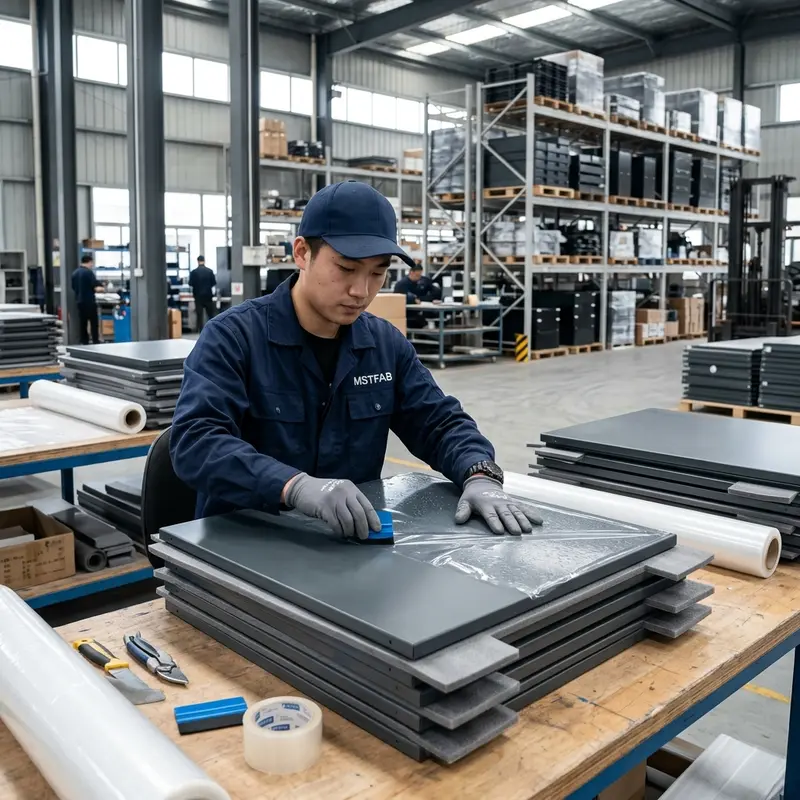
- Put on the quality plan: finished checks, sample size, packing materials and protected zones.
- Ask for evidence: inspection results and packing photographs before shipment.
- Red flag: coating is approved before mask removal, assembly checks and packing.
Copy-and-Paste Powder Coating Drawing Notes
The buyer’s engineering and quality teams should approve project-specific values, but controlled notes can follow this structure:
- Apply the specified pretreatment and powder-coating system to the surfaces identified on the released drawing.
- Mask grounding pads, bonding zones, threads, gasket interfaces and functional mating surfaces according to the controlled masking map.
- Coating shall not obstruct specified threads, removable panels, door operation, latch engagement or component cutouts.
- Finished coating thickness shall be measured at the locations and sampling level defined by the quality plan.
- Cosmetic surfaces shall be evaluated by the approved class, lighting, viewing distance and finish sample.
- Finished first-article inspection shall verify appearance, masks, functional fit and packaging protection before production release.
Supplier Responsibility Matrix
| Project item | MSTFAB fabrication scope | Buyer or integrator scope |
|---|---|---|
| Enclosure geometry | Manufacture to released drawings | Define interfaces, components and acceptance criteria |
| Powder-coating process | Apply contracted finish and inspection | Define environment and performance requirements |
| Masking map | Apply approved masks to controlled geometry | Define bonding, sealing and functional zones |
| Threads and installed hardware | Protect and inspect specified features | Define sequence, torque and component requirements |
| Cosmetic acceptance | Inspect to approved classes and samples | Approve zones, samples and rejection limits |
| Electrical and telecom system | Not included in standard sheet metal scope | Own design, validation and final compliance |
When to Request a Coating and Masking DFM Review
Request review before quotation when the enclosure has multiple grounding pads, dense threaded hardware, tight rack interfaces, large gasketed doors, removable gland plates, connector cutouts, outdoor corrosion requirements or highly visible Class A surfaces. Send the STEP assembly, dimensioned PDF, material, finish specification, color and texture sample, masking map, quantities and first-article requirements.
MSTFAB provides drawing-based custom telecom enclosure fabrication for empty cabinet shells and mechanical structures. We can review coating access, mask geometry, finished clearances, hardware sequence, cosmetic zones and mechanical inspection. Submit controlled project files through the MSTFAB contact page.
Frequently Asked Questions
How much thickness does powder coating add to a telecom enclosure?
There is no universal value. Thickness depends on the powder system, geometry, application method and project specification. Buyers should define the acceptable range and measurement locations, then include coating on all relevant mating surfaces in the tolerance review.
Should all grounding points be masked before powder coating?
Only grounding or bonding interfaces identified by the approved electrical design should be masked. The drawing should define exact geometry and location. The OEM or integrator must validate the completed bonding path after assembly.
Can coated threads simply be cleaned with a tap?
Thread chasing is controlled rework, not an automatic substitute for masking. It can create debris and remove corrosion protection around the feature. If permitted, the drawing or process plan should define the method and inspection requirement.
Should gasket lands be coated or left bare?
That depends on the gasket material, sealing design, corrosion strategy and adhesion method. The buyer should define the required surface condition. The important point is that the complete sealing path is controlled and inspected consistently.
Why does a gland plate fit before coating but bind afterward?
The plate edge and cabinet opening may both receive coating, reducing total clearance. Masking edges can also create local ridges. Review the finished stack-up and verify insertion and removal on the coated first article.
What should an OEM send for a powder-coating DFM review?
Send the complete enclosure model, released drawings, substrate, finish system, color and texture requirements, coating-thickness range, masking map, grounding and gasket interfaces, cosmetic-zone definitions, quantities and required first-article evidence.
 WeChat Contact
 WhatsApp Me Directly