
⚡ Direct Answer: How to Minimize Tooling Costs (NRE) on Low-Volume Sheet Metal Parts?
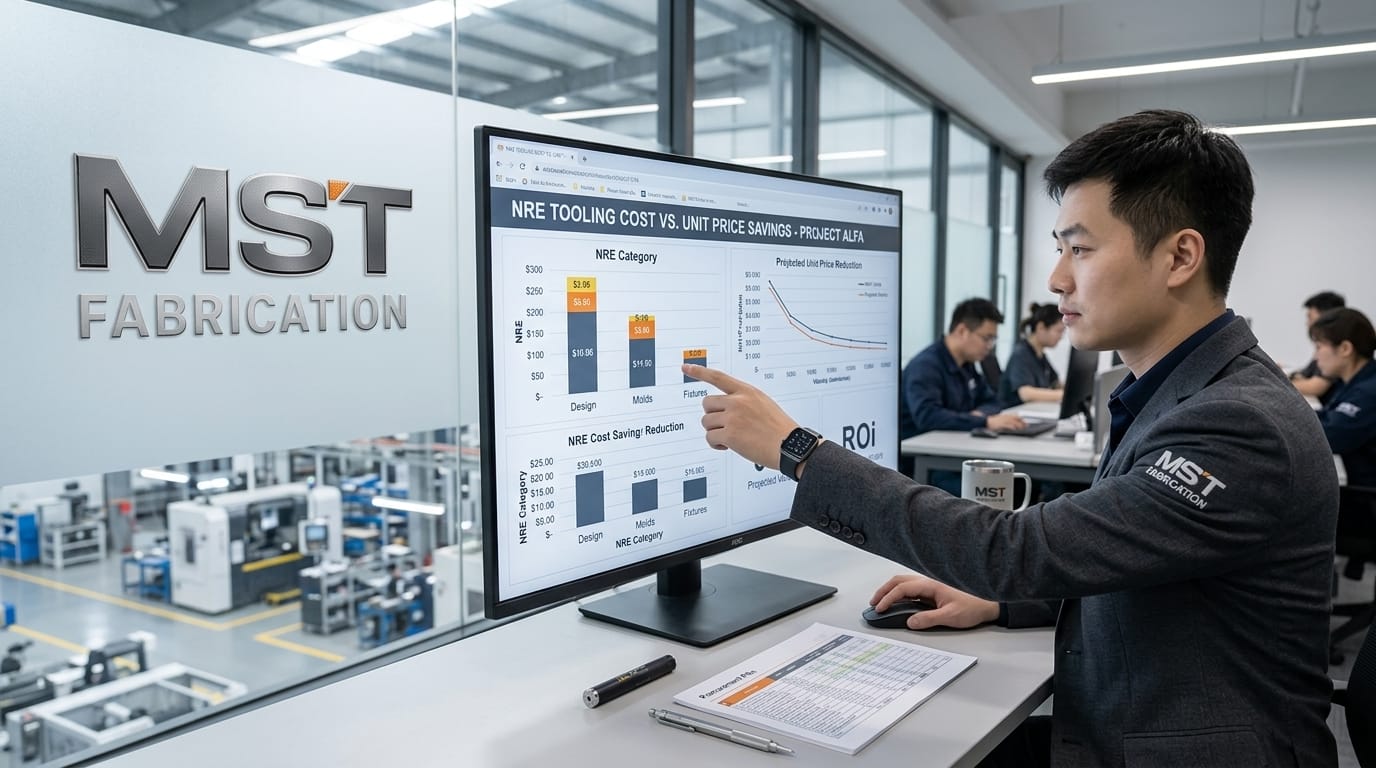
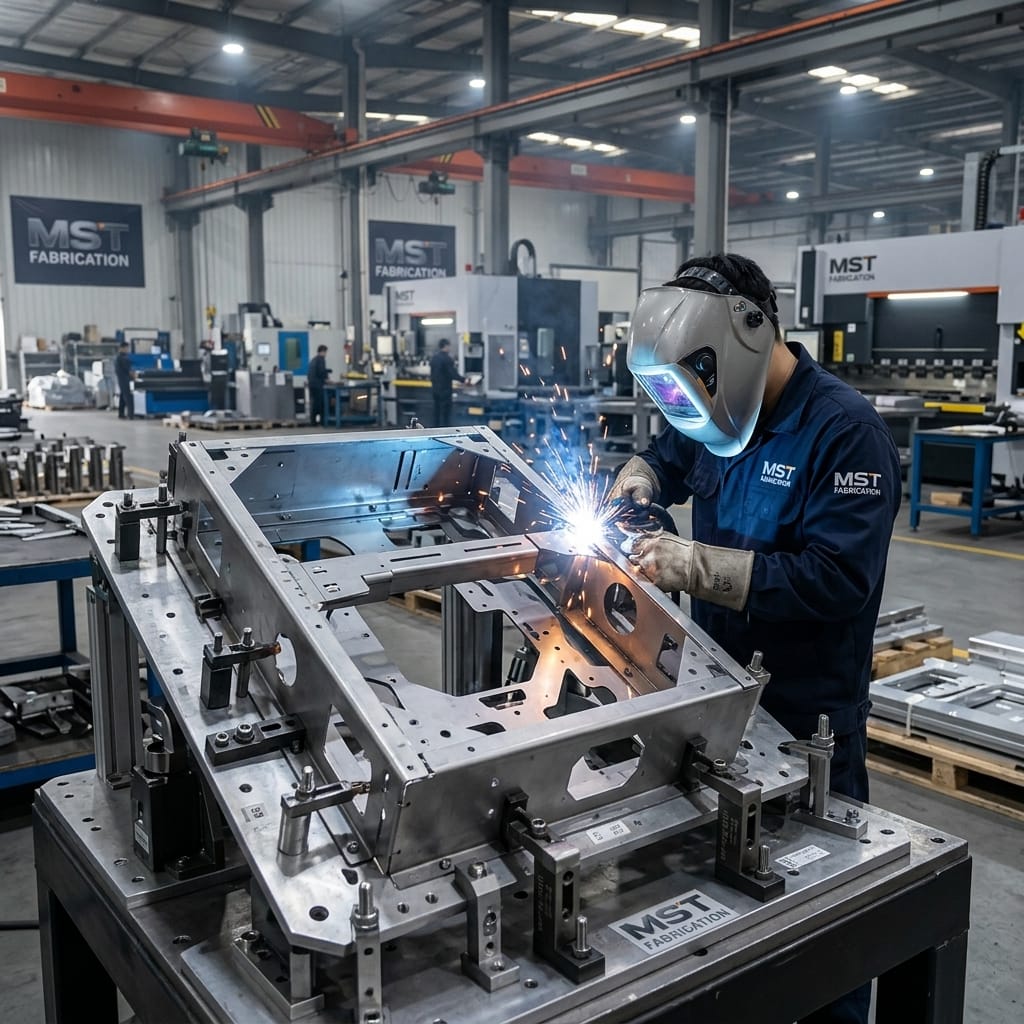
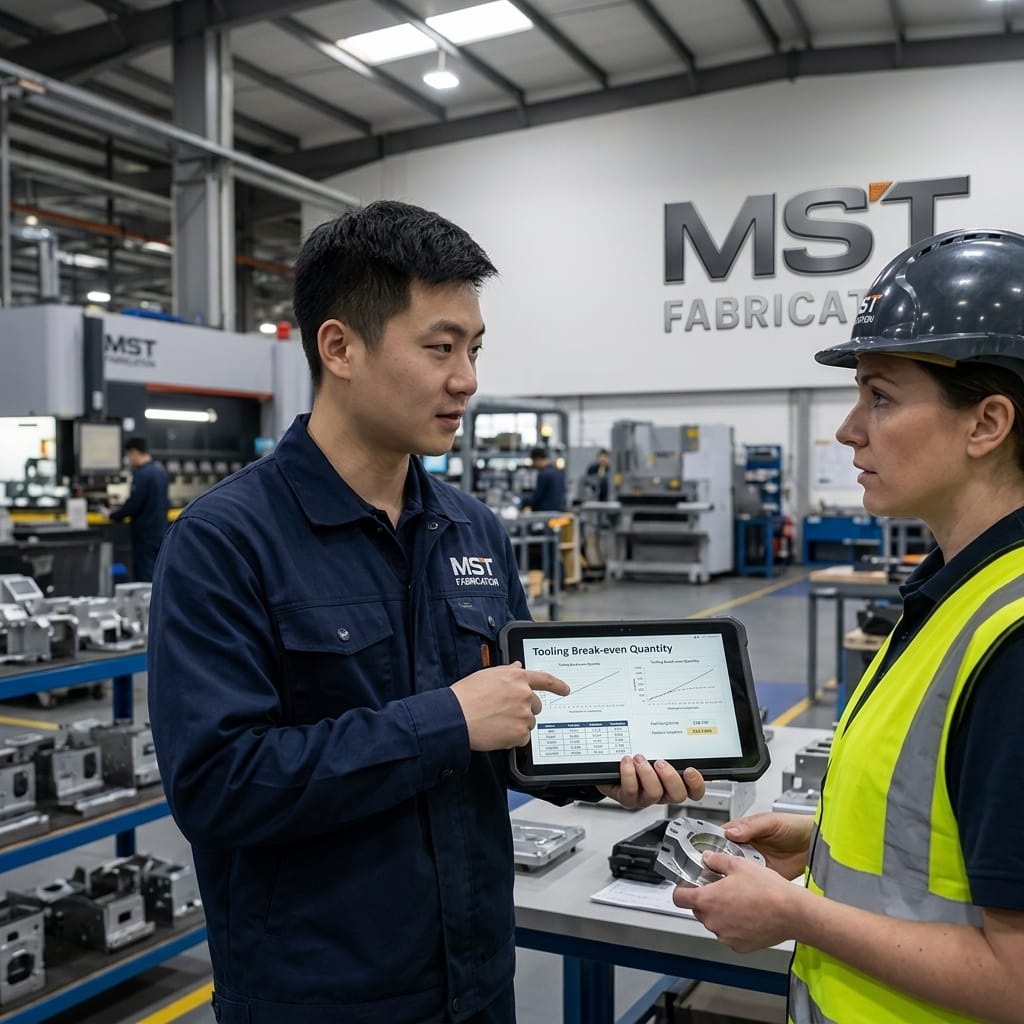
Minimizing Non-Recurring Engineering (NRE) and tooling costs for low-to-mid volume sheet metal parts (50 to 2,000 units annually) relies on 4 smart tooling decisions: 1) Soft Tooling Architecture (Zero NRE): Utilizing high-speed fiber laser cutting and multi-axis CNC press brakes with standard segmented punches and V-dies, completely avoiding 15,000–40,000 progressive stamping dies; 2) Modular Welding Jigs: Assembling temporary clamping fixtures using 3D modular welding tables with re-usable toggle clamps (500–1,200 NRE vs 8,000 dedicated hard fixtures); 3) Break-Even Volume Modeling: Transitioning from CNC press brake air-bending to hard progressive dies only when annual volumes exceed 5,000 to 10,000 pieces; and 4) Off-the-Shelf Standard Hardware Tooling: Designing around catalog self-clinching PEM fasteners that utilize universal punch anvils rather than custom clinch dies.
Tooling Cost (NRE) vs Piece-Price Economic Break-Even Analysis
| Manufacturing Method | Upfront Tooling NRE Cost | Piece-Price Benchmark | Optimal Annual Volume |
|---|---|---|---|
| 1. CNC Laser & Press Brake (Soft Tooling) | 0 (Zero Tooling Fee) | Moderate (18.50 / part) | 10 to 2,500 pieces per year |
| 2. Semi-Dedicated Form Tooling | 1,500 – 3,500 (Custom V-die / punch) | Low-Moderate (12.00 / part) | 2,500 to 7,500 pieces per year |
| 3. Progressive Stamping Hard Die | 25,000 – 60,000 (Hard tool steel) | Lowest (3.80 / part) | 10,000+ pieces per year |
| 4. Dedicated Welding / Check Fixture | 800 – 2,000 (Modular aluminum) | Reduces weld cycle time by 40% | 100+ welded assemblies |
In custom equipment manufacturing, absorbing a 30,000 progressive die cost across an annual production volume of 500 equipment covers adds an unacceptable60 per part in tooling amortization alone. By optimizing part designs for CNC laser profiling and multi-stage press brake bending, MSTFAB enables equipment OEMs to manufacture intricate, high-precision sheet metal parts with zero upfront tooling charges and zero risk of design obsolescence.
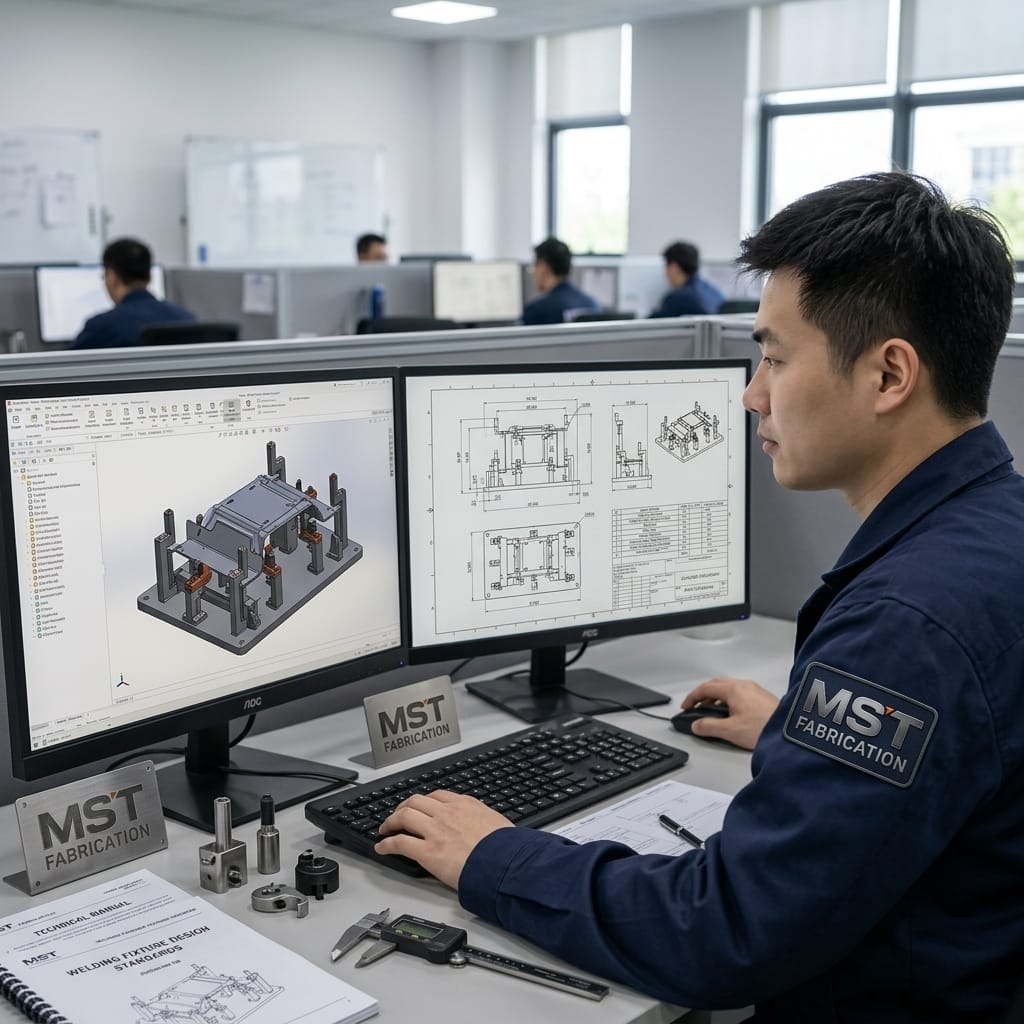
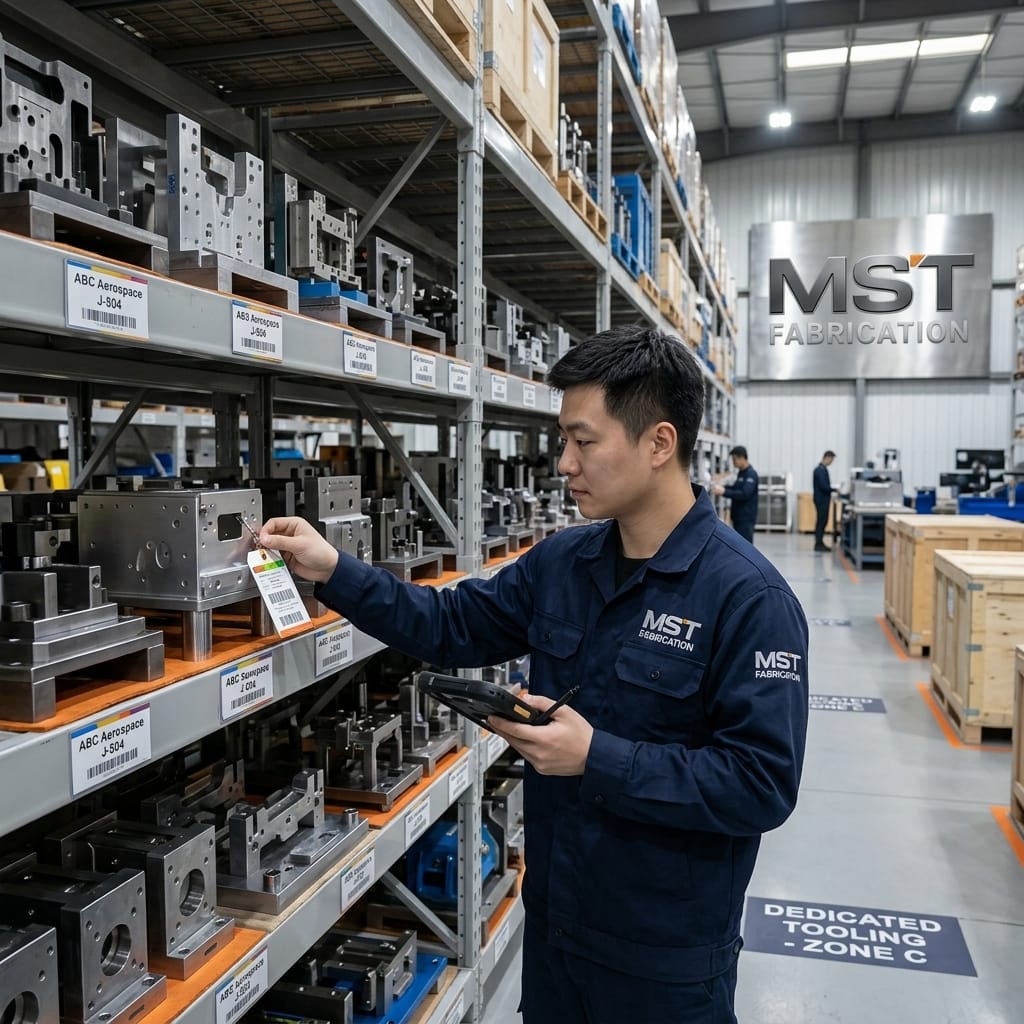
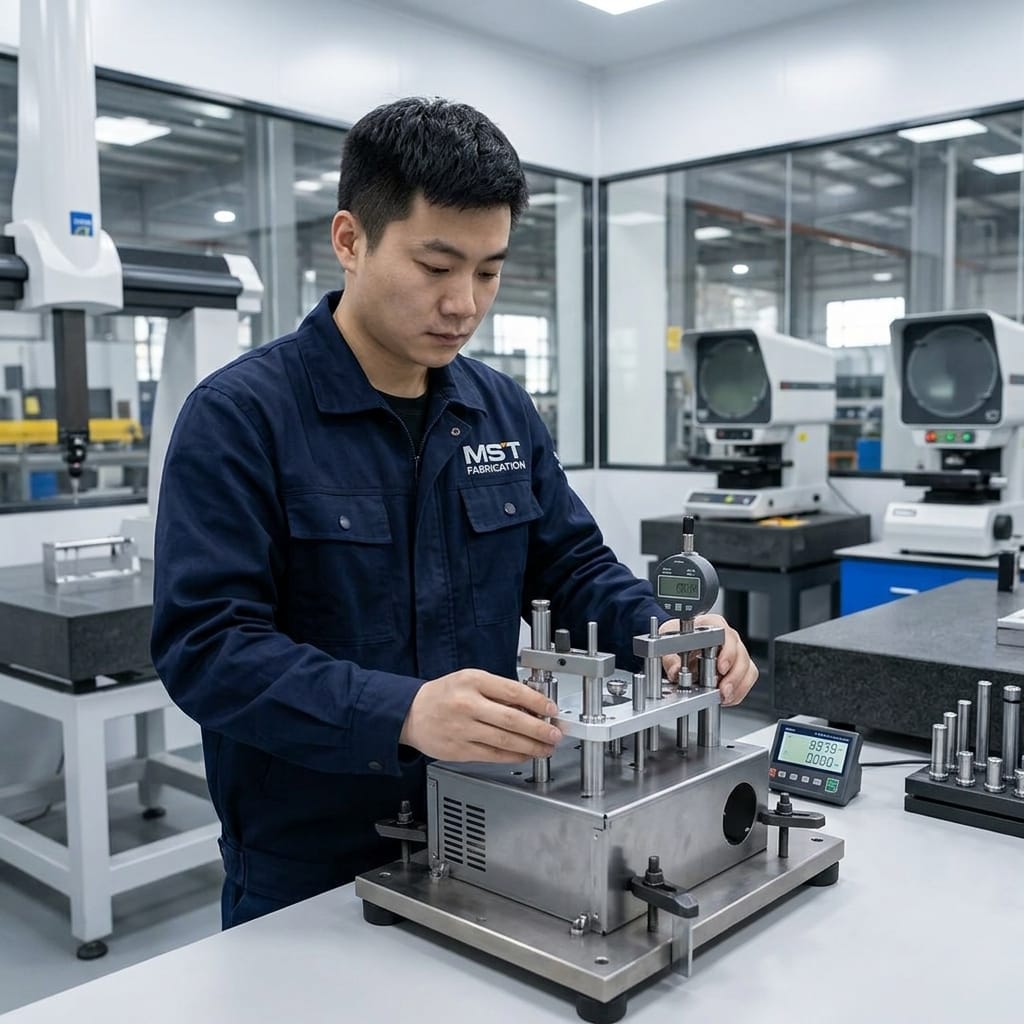
Fixture Design, Forming Tools & Dedicated Checking Gauges
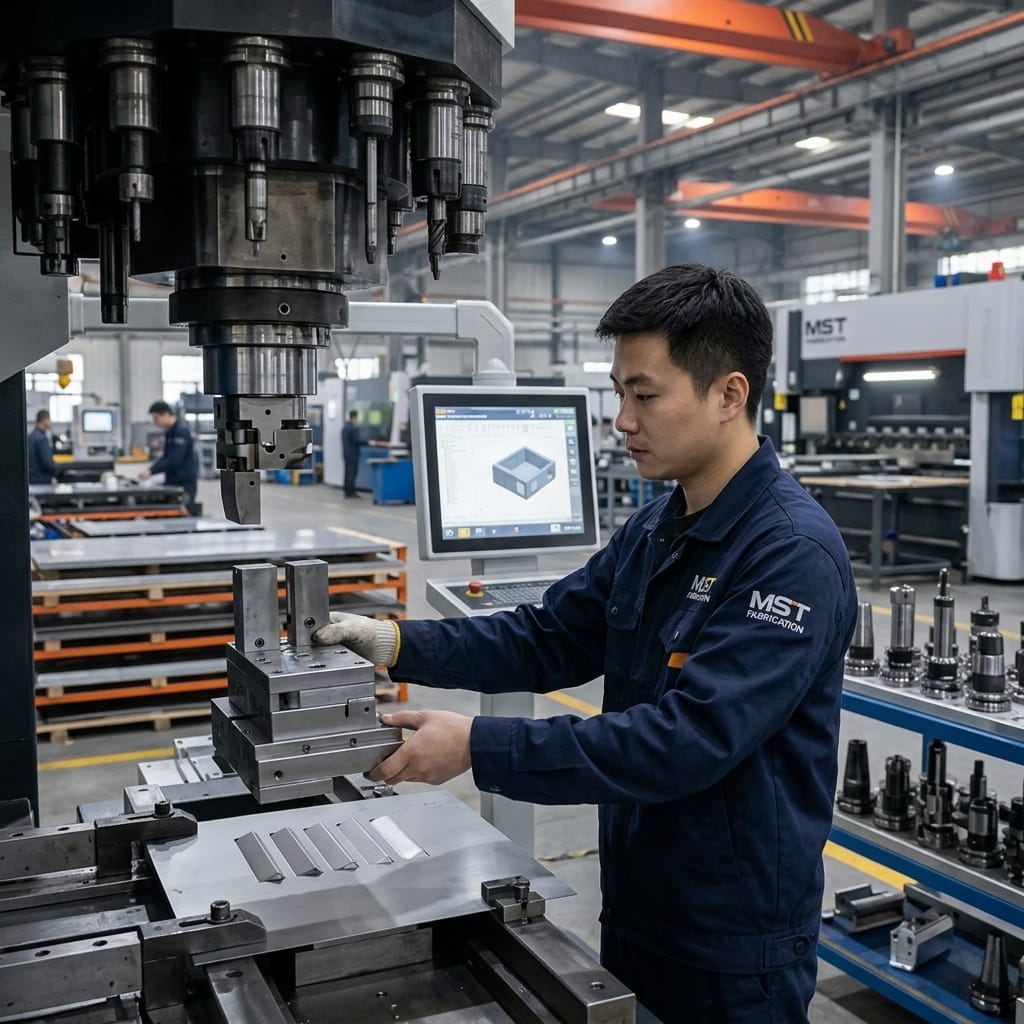
When low-volume projects require specialized features—such as custom louvers, deep card guides, or tight radius return lips—MSTFAB designs modular forming inserts that mount directly into standard press brake tool holders. This delivers custom formed geometry at less than 10% of dedicated die costs.
Manufacture Custom Sheet Metal Parts Without Massive Tooling Fees
Send your STEP models to MSTFAB for complete soft-tooling feasibility analysis. We calculate break-even volumes and manufacture parts with zero die NRE.
Frequently Asked Questions on Low-Volume Tooling Costs
What is NRE in sheet metal manufacturing?
NRE stands for Non-Recurring Engineering. It covers one-time upfront costs—such as dedicated CNC programming, custom press brake tooling, welding fixture design, and FAI report setup—that are paid once and not repeated on re-orders.
How do design changes affect low-volume soft tooling?
With soft tooling (laser cutting and CNC press brake), design changes require only a quick update to the CAD/CAM program with zero tooling scrap or die modification fees, making it ideal for evolving products.
 WeChat Contact
 WhatsApp Me Directly