
What physical evidence should auditors evaluate during a sheet metal supplier factory audit?
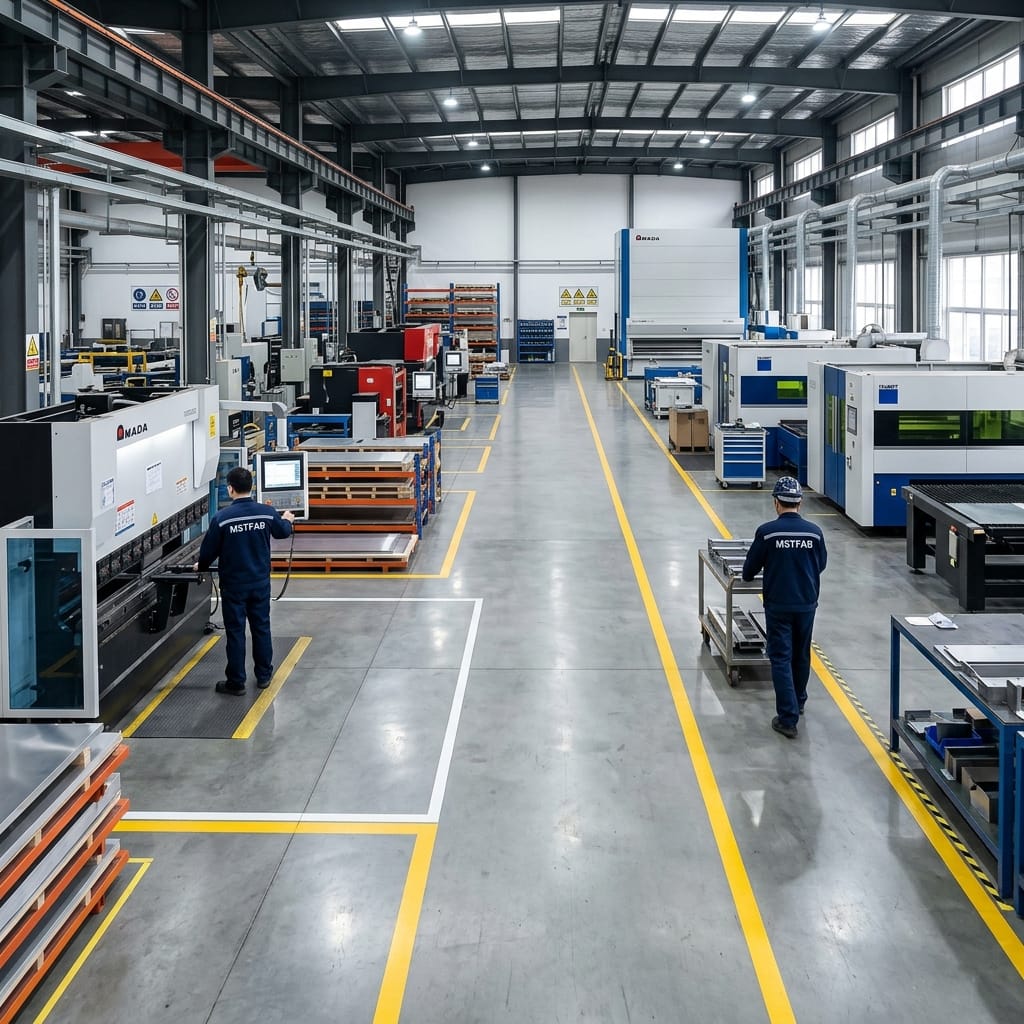
A sheet metal supplier audit checks whether a factory can repeatedly make your drawing-defined parts and prove the result. Follow one representative job from material receipt through cutting, bending, welding, hardware installation, finishing and release. Compare the drawing revision, process records, measuring methods, subcontracted work and corrective actions against the requirements in your RFQ.
Start with a representative part, its current drawing and the acceptance plan. A tidy workshop is useful, but it does not prove that the mounting holes fit. Ask the supplier to show how the same revision reaches purchasing, machine setup, inspection and packing. Record each finding with the evidence, project risk, responsible person and closure date.

Five Evidence Areas for a Sheet Metal Supplier Audit
1. Raw Material Receiving & Traceability
Select a stored sheet, cut blank or work-in-progress part and trace it to the receiving record and job. Check grade, thickness, identification and segregation of different materials. When the order requires a mill certificate or heat/lot traceability, verify that the document identifies the supplied material. Agree the required retrieval method and response time rather than applying an arbitrary three-minute pass/fail rule.

2. Cutting, Bending & Measurement Control
Review maintenance and setup checks appropriate to the equipment, manufacturer instructions and job risk. Then ask how the supplier verifies a representative cut profile and formed part against the drawing. Measuring tools must be suitable for the tolerance and measurement method, with their verification or calibration status controlled where required. A CMM or a particular machine brand is not a universal prerequisite.

3. Revision, Tooling & Nonconforming-Part Control
Compare the production traveler, drawing, CAM program and setup record for the same job. Check that tooling is identified, protected from damage and appropriate for the specified material and geometry. Ask how obsolete instructions are removed and suspect parts are kept from approved stock. Review one nonconformance from detection through disposition and corrective action.
4. Welding, Hardware & Outsourced Finishing
Where relevant to the part, review weld access, distortion control, fastener part numbers, installation conditions and finish masking. Identify who performs each operation. Request weld, hardware-retention or coating tests only when the drawing or purchase specification requires them, and agree the method, sample quantity and acceptance limits before pricing.
5. First Article, Packing & Corrective Action
Review how the supplier records critical dimensions and fit, obtains approval for deviations, and protects visible surfaces during packing. Check one completed job rather than relying on an empty report template. A successful sample does not remove the need for production inspection and change control.
On-Site Sheet Metal Supplier Audit Evidence Matrix
Use this matrix to agree the audit scope. The buyer sets risk-based acceptance criteria; the categories are not a universal certification or a fixed percentage score.
| Audit Area | Check on a Representative Job | Evidence to Request | Finding to Resolve | Before Order Release |
|---|---|---|---|---|
| 1. Quality & revision control | Current drawing, order requirements and deviation approval | Released traveler, change record and relevant corrective-action example | Shop-floor instructions do not match the released revision | Agree document precedence and change authorization |
| 2. Material identification | Grade, thickness and required lot continuity | Receiving record and matching material certificate when specified | Different grades mixed or required identity lost after cutting | Define certificate type and required traceability depth |
| 3. Manufacturing route | Cutting, forming, welds and hardware against the actual geometry | Representative setup and in-process records; equipment maintenance plan | A critical feature has no practical control or checking method | Confirm in-house work, partner work and process limits |
| 4. Inspection & disposition | Datums, critical dimensions, fit and handling of rejected parts | Agreed FAI/check sheet, suitable gauges and required calibration status | No agreed acceptance limits or unresolved rejected parts in approved stock | Define inspection scope, sampling and approval responsibility |
| 5. Finishing & shipment | Masking, appearance, finish checks and protective packing | Finisher identity, agreed test records and packing example | Outsourced finishing is undisclosed or required records are unavailable | Confirm finish route, test method and shipment evidence |

Define the Audit Scope With Your Drawing
Send a representative STEP/PDF package, material, quantity, finish and critical acceptance requirements. MSTFAB will review the drawing-based metalwork scope and confirm which records and audit arrangements can be provided. Surface treatments may involve qualified long-term partners; their role and any required test evidence must be agreed before the order.
For the inspection handoff, use the quality control workflow. Before quotation, confirm the drawing package and manufacturing scope on our sheet metal fabrication page.
 WeChat Contact
 WhatsApp Me Directly