
PEM Fasteners Installation Guide: How Do You Prevent Spin-Out and Sheet Distortion?
Reliable self-clinching PEM fastener installation requires holding laser-cut mounting holes within +0.08 mm/-0.00 mm (+0.003″/-0.000″), respecting minimum centerline-to-edge distance, and pressing fasteners with a flat parallel hydraulic punch into bare or pre-plated metal before powder coating.
- Mounting Hole Tolerance: Cut or punch mounting holes to +0.08 mm / -0.00 mm without deburring or chamfering; chamfered edges prevent the clinching ring from biting into parent metal.
- Hardness Differential Rule: Parent sheet hardness must remain below HRB 80 for standard carbon steel PEM nuts (CLS/S) and below HRB 70 for stainless steel panels unless hardened SP (400-series SS) fasteners are specified.
- Minimum Sheet Thickness & Edge Distance: Standard M3–M6 self-clinching nuts require ≥0.8 mm to 1.4 mm sheet thickness and ≥5.6 mm to 8.6 mm minimum centerline-to-edge or bend-tangency clearance.
- Sequence Relative to Powder Coating: Install PEM hardware before powder coating and mask internal threads with silicone plugs so anodize or 80 μm powder film never compromises push-out or torque-out strength.
🔩 Direct Answer: What Is Sheet Metal Fabrication with PEM Hardware Installation?
Sheet metal fabrication with PEM hardware installation is the manufacturing integration of self-clinching fasteners (PennEngineering standard threaded nuts, studs, standoffs, and captive panel screws) into sheet metal components using hydraulic/pneumatic insertion presses. Under controlled compressive force, the fastener’s serrated clinching ring displaces sheet metal into an undercut groove, permanently locking the hardware with high push-out force (>500 N) and torque-out resistance (>5 Nm) without heat, distortion, or weld spatter.
Common Self-Clinching PEM Fasteners in OEM Enclosures
| PEM Fastener Type | Thread Size Range | Installation Mechanism | Typical Enclosure Use |
|---|---|---|---|
| Self-Clinching Nuts (Type S / CLS) | M2 to M10 (#2-56 to 3/8-16) | Parallel squeezing press forces serrations into sheet. | Strong load-bearing internal threads on thin sheet metal. |
| Flush-Head Studs (Type FH / FHS) | M3 to M8 (#4-40 to 5/16-18) | Head finishes completely flush with exterior sheet metal skin. | Mounting exterior displays, handles, and PCB boards without visible screw heads. |
| Through-Hole Standoffs (Type SO / SOS) | M2.5 to M5 (#4-40 to #10-32) | Hexagonal head provides high rotational torque resistance. | Stacking circuit boards, sub-chassis spacing, component standoff mounts. |
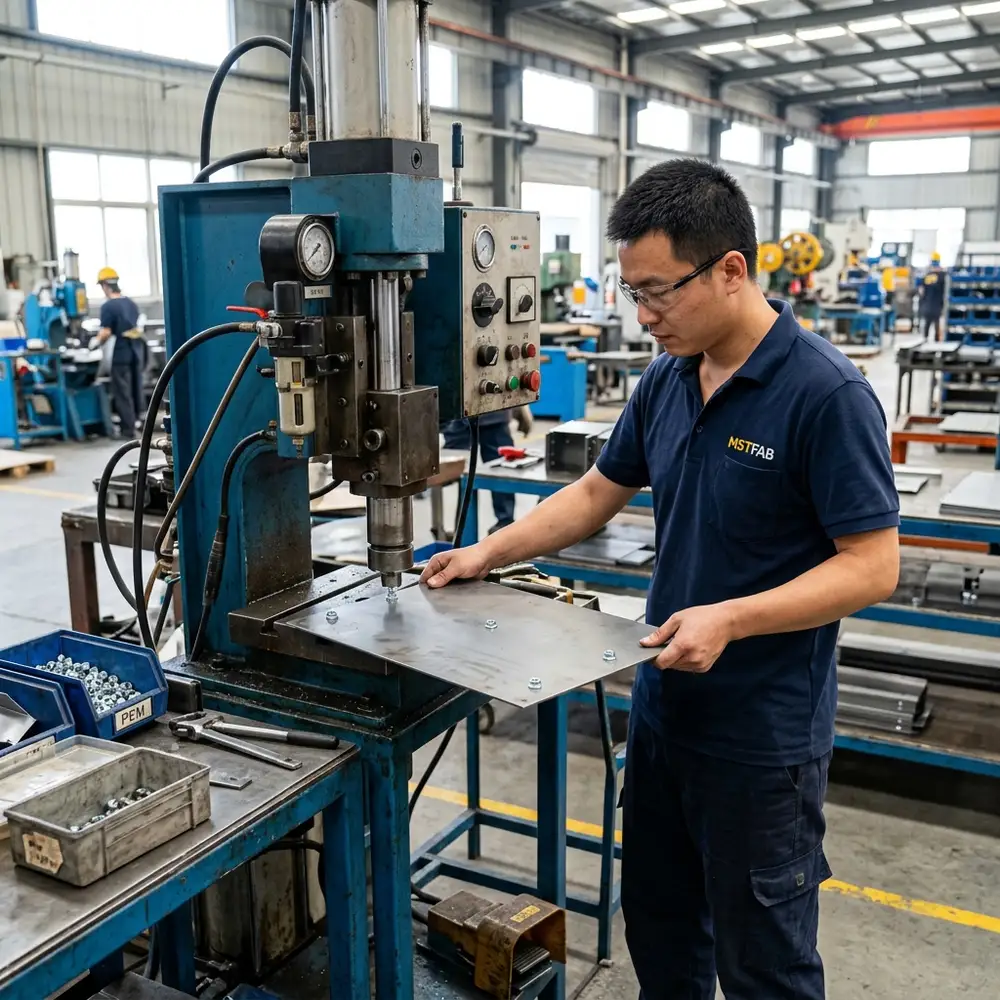
Integrate Self-Clinching PEM Fasteners
Send your sheet metal drawings to MSTFAB. We review mounting hole punch sizes, minimum centerline-to-edge margins, and provide quotes within 24 hours.
Frequently Asked Questions on PEM Hardware
Can PEM hardware be installed before powder coating?
Yes. We routinely install PEM studs and nuts prior to coating. Internal female threads and external male studs are protected using high-temperature silicone masking plugs and caps to prevent powder buildup inside threads.
 WeChat Contact
 WhatsApp Me Directly