AUTOMOTIVE EQUIPMENT SHELL QUALITY CONTROL
Automotive enclosure change control uses an engineering change notice (ECN), supplier change request and risk-based reapproval to stop an approved sheet metal shell from quietly becoming a different part. For automotive automation control boxes and machinery enclosures, the buyer should control 4M changes, affected CTQs, revision effectivity and old-stock disposition before repeat production moves.
THE QUICK ANSWER
Control changes by risk, not by how small they look
Use a controlled ECN or supplier change request. Classify whether the proposal changes people or qualifications, machine or tooling, material or source, manufacturing method or the approved product definition. Map the affected CTQs, agree the partial FAI or PPAP evidence and obtain buyer approval before implementation.
- Freeze one released model, drawing, BOM and finish package.
- Screen the proposal for 4M and product-definition risk.
- Define affected CTQs, evidence and approval authority.
- Set the effective revision, date, quantity and old-stock disposition.
ECN, PCN and 4M Change: What Automotive Buyers Mean
These terms overlap, but they are not interchangeable. Define them in the purchase agreement so the supplier knows which record to open, who approves it and whether the change is temporary or permanent.
| Record or screen | Typical initiator | What it controls |
|---|---|---|
| ECN / engineering change notice | OEM, integrator or design authority | A released design or specification revision, its effectivity and the parts or orders it changes |
| Supplier change request | Fabricator or approved subcontractor | A proposed material, source, machine, tooling, method, site or inspection change before implementation |
| PCN / process change notification | Material, hardware or process supplier | An upstream product or process change that may flow into the enclosure BOM or approved manufacturing route |
| 4M change review | Buyer and supplier quality teams | A risk screen for people, machine, material and method changes; many teams separately add measurement and environment |
| Temporary deviation | Either party | A limited quantity or time-bound exception with expiry, containment and disposition |
Change Control Is Not the Same as PPAP or IATF Certification
This page has a narrower search intent than MSTFAB’s PPAP and IATF guides. It explains the buyer-supplier approval path for mechanical enclosure changes. It does not decide whether a project requires a full automotive production-part approval process or whether a particular supplier must hold IATF 16949 certification.
An enclosure used on a robotic cell, vision station or battery-module assembly machine usually remains factory equipment. It does not automatically become a vehicle production part. The OEM should define the contractual quality requirements based on the real application, customer-specific requirements and risk. Our automotive machinery control box IATF quality flow-down guide shows how buyer requirements can become drawing notes, CTQs and retained evidence without inventing a certification claim.
When a project does require production-part-style evidence, our PPAP guide for automotive automation enclosure shells explains a suitable evidence package without turning every door hinge into a doctoral thesis.
Configuration control
One approved drawing, model, BOM, finish specification and deviation history.
Change notification
A written request before implementation, with affected parts and reason.
Reapproval evidence
Only the documents, samples and tests needed to address the changed risk.
Begin with a Controlled Baseline
Change control cannot work if nobody can identify the approved condition. The baseline should connect the purchase order to the released STEP model, dimensioned PDF drawings, hardware list, finish specification, inspection plan and approved deviations. A practical automotive control box shell quality plan then ties each critical-to-quality characteristic to its method, frequency, record and reaction plan.
Part number and revision must agree across every file. Names such as final-final-use-this-one.step communicate emotion, not configuration.
| Baseline item | What to control | Approval evidence |
|---|---|---|
| 3D assembly | Geometry, interfaces, keep-outs and installed orientation | Released file ID and revision |
| 2D drawings | Datums, CTQs, tolerances, welds and hardware | Signed or workflow-approved release |
| Finish specification | Pretreatment, color, texture, thickness and masking | Controlled specification and sample |
| Inspection plan | Methods, stage, sampling and report format | Approved FAI or control plan |
| Deviation log | Temporary acceptance, quantity and expiry | Buyer authorization and closure |

4M Change Matrix for Automotive Enclosure Suppliers
4M is a fast risk screen, not an automatic order for full PPAP. Review the proposed change against the enclosure interfaces it can influence, then request only the evidence needed to close that risk.
| 4M category | Enclosure examples | Proportionate evidence |
|---|---|---|
| People | New qualified welder, inspector or coating technician on a controlled operation | Training or qualification record, first-off review and targeted audit where the contract requires it |
| Machine | Different laser, press brake, welding cell, fixture, coating line or measurement system | Machine or fixture comparison, capability check and affected CTQ results |
| Material | Grade, thickness, mill source, hinge, latch, PEM hardware or coating chemistry | Certificate or datasheet comparison, sample fit and corrosion or finish evidence where relevant |
| Method | Bend sequence, weld map, masking route, inspection setup, packing method or subcontracted step | Updated work instruction, risk review, control-plan change and partial FAI on affected features |
Many automotive teams use 5M or 6M by adding measurement and environment. The label matters less than ensuring the contract catches every change that can affect fit, function, appearance, traceability or prior approval.
Use Three Approval Levels After the 4M Screen
A practical classification avoids two bad extremes: approving nothing, or requiring a committee meeting whenever a cutting nozzle is replaced. The buyer and supplier should agree examples before production.
| Level | Typical examples | Required action |
|---|---|---|
| A: Administrative | Contact name, document format or typo with no technical effect | Record and communicate; no product reapproval |
| B: Process | Fixture maintenance, equivalent machine or inspection equipment change with no intended product change | Supplier risk review and defined verification; notify if contract requires |
| C: Product or approved construction | Material, thickness, hardware, geometry, weld, finish, subcontractor or acceptance method | Written buyer approval before production or shipment |
Drawing and Interface Changes
Changes to the enclosure body, door, removable panel, gland plate, mounting plate or bracket can create an interface mismatch even when each individual part looks reasonable. Review the complete assembly relationship.
Typical triggers include moved holes, changed cutout radii, altered bend deductions, new cable entries, different door gaps, revised mounting patterns and a STEP model that no longer matches the drawing. Email instructions should be incorporated into the controlled release instead of becoming permanent archaeology.
Material and Thickness Changes
A change from cold-rolled steel to zinc-coated sheet, one galvanized grade to another, a reduced thickness or an alternative stainless or aluminum grade can affect stiffness, forming, welding, hardware installation, corrosion behavior, weight and coating.
The supplier change request should identify the current and proposed callouts, source, reason and affected characteristics. Evidence may include a material certificate, thickness record, bend sample, weld sample or updated first article. The correct evidence proves the requirement; the wrong evidence mostly proves that email attachments can be large.
Hardware Substitutions Need More Than Matching Hole Centers
Hinges, latches, handles, studs, PEM hardware, rivet nuts and fasteners may look interchangeable while differing in material, plating, grip range, load, compression, keying, corrosion resistance or installation force.
A proposed alternative should include a datasheet, dimensional comparison, material/finish comparison, sample fit and any required life or load evidence. Procurement should also confirm whether the alternative becomes the new approved source or only covers a temporary shortage.

Weld, Fixture and Joint-Design Changes
Weld sequence, fixture location, seam length and joint design can affect frame squareness, door fit, mounting patterns and cosmetic surfaces. A change intended to save time may also move heat into a less friendly location.
Review updated weld maps, fixture changes, distortion controls and post-weld inspection. Where a tab, fastener or folded return replaces a weld, confirm strength, access, corrosion protection and the approved appearance.

Mounting Plate and Bracket Changes
Moving a mounting plate two millimetres may sound harmless until cable clearance, DIN-rail position or service access disappears. Control plate size, flatness, hole pattern, stud height, stand-off position and installed clearance as a system.
When the customer installs components later, provide a keep-out model, interface drawing or representative gauge. MSTFAB can check mechanical fit; the customer remains responsible for electrical design, component spacing and the performance of the completed system.
Surface Finish, Masking and Subcontractor Changes
Powder-coating supplier, pretreatment route, color source, texture, coating thickness and masking method can affect adhesion, appearance, grounding points, threads and tight fits. A supplier-site or subcontractor change should be assessed against the characteristics that process controls. The approved route should use the same measurable requirements defined for sheet metal surface treatment, including pretreatment, color, texture, thickness, masking and adhesion evidence.
Do not ban subcontracting by reflex. Define what may be subcontracted, which controls apply, what evidence is retained and when a new source requires approval. Hidden subcontracting is the problem; a controlled specialist process is simply part of the supply chain.
Inspection-Method Changes Can Change the Answer
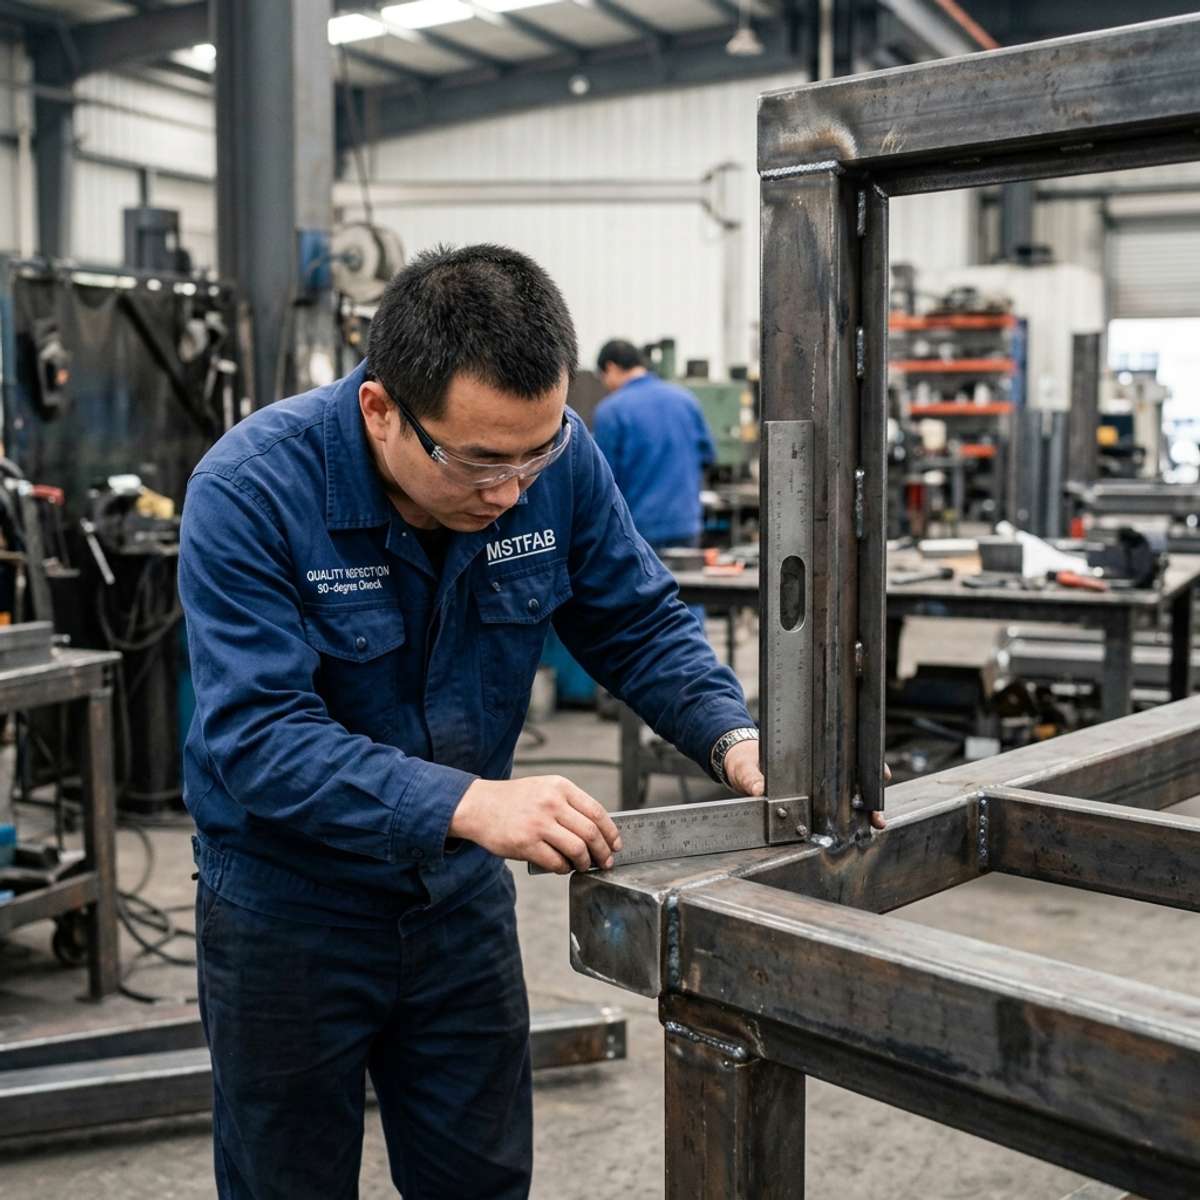
A characteristic measured with a steel rule, caliper, fixture or CMM may produce different uncertainty and interpretation. Changing the datum setup, sample size or inspection stage can make results look different without changing the metal.
Control the method for critical door gaps, flatness, mounting patterns, cutouts, hardware and after-finish interfaces. If a new method is proposed, compare it against the approved method on representative parts.
Automotive Supplier Change Request Checklist
A useful supplier change request, PCN or ECN response should answer six questions without making procurement chase five separate email threads.
Describe the change
Current condition, proposed condition, reason and planned implementation date.
Identify the scope
Affected part numbers, revisions, open orders, inventory and subcontracted processes.
Assess the risk
Fit, function, appearance, traceability, assembly, packaging and previous approval evidence.
Submit evidence
Redlined drawings, certificates, samples, FAI results, photos or process comparison.
Obtain approval
Named buyer authority, approval status, conditions and effective quantity/date.
Update records
Released files, shop instructions, control plan, inventory identity and revision history.
When Does an ECN or 4M Change Require New FAI or PPAP?
A new or partial FAI is appropriate when the change can affect a previously approved characteristic. It does not always require measuring every dimension again. Link the reapproval scope to the changed risk.
For a compact example where a small interface change can alter assembly fit, see the IATF 16949 automotive switch box release guide. It covers the actuator cutout, anti-rotation features, rear clearance and first-article checks before the shell baseline is released.
| Change | Typical reapproval evidence | Buyer decision |
|---|---|---|
| Drawing geometry | Redline, affected CTQs and trial fit | Approve revised product definition |
| Material or thickness | Certificate, thickness, forming/weld checks and affected CTQs | Approve material and performance risk |
| Hardware | Datasheet comparison, fit and functional evidence | Approve permanent or temporary source |
| Weld or fixture | Weld review, squareness, gap and flatness results | Approve process or construction change |
| Finish supplier | Color, thickness, adhesion, masking and sample | Approve appearance and process evidence |

A Purchase-Order Clause Buyers Can Adapt
This is practical drafting, not legal advice. Align the final clause with the purchase agreement, customer-specific requirements and the buyer’s quality system.
Supplier Responsibility Matrix
| Activity | OEM or integrator | MSTFAB |
|---|---|---|
| Product definition | Approve design, interfaces, material and acceptance criteria | Review manufacturability and build to released files |
| Change classification | Define contractual notification and approval rules | Assess proposed fabrication changes and notify as required |
| Validation scope | Approve evidence and finished-equipment risk | Produce agreed samples, FAI and mechanical records |
| Electrical system | Components, wiring, testing, programming and certification | No finished electrical-equipment scope |
| Release to production | Approve or reject the change | Implement only the approved effective revision |
Packaging and Identification Changes Matter Too
Changed protective film, separators, pallet pattern, labels or stacking limits can create scratches, moisture damage or traceability gaps. Define part and revision labels, quantity per pack, corrosion protection and separation of unlike revisions.
A correct enclosure in the wrong labeled crate is still an expensive logistics puzzle.

Common Buyer Mistakes
- Sending a new model without withdrawing the old release
- Approving prototype handwork but never updating production drawings
- Writing “no changes” without defining which changes require notification
- Demanding full PPAP for every low-risk administrative change
- Allowing email deviations to become permanent manufacturing instructions
- Approving a substitute by price and hole pattern only
- Measuring changed CTQs with a different, undocumented method
- Mixing old and new revisions in inventory or packaging
Standards and Responsibility Boundary
ISO quality-management guidance supports controlling documented information and recording review, authorization and actions for changes. Automotive customer requirements may add stricter notification, supplier-development or approval obligations. The purchase contract and customer-specific requirements decide the applicable evidence.
A certificate demonstrates a management-system scope; it does not approve an enclosure revision, hardware substitution or process change on the customer’s behalf.
Official references: ISO guidance on documented information and IATF stakeholder communiques.
Frequently Asked Questions
What is a 4M change in automotive manufacturing?
A 4M change affects people or qualification, machine or tooling, material or source, or manufacturing method. It is a risk-screening category, not automatic proof that full PPAP is required. The buyer should connect the changed category to affected CTQs and proportionate reapproval evidence.
What is the difference between an ECN and a supplier change request?
An ECN normally releases a buyer-controlled design or specification revision. A supplier change request asks permission to alter a source, process, machine, tooling, site or inspection method. Both records need affected parts, effectivity, validation evidence and named approval.
Does moving production to another machine require PPAP?
Not always. Compare the machine, tooling, program, fixture and measurement route against the approved process. If the move can affect previously approved characteristics or the customer contract lists it as a notification trigger, perform the agreed partial or full reapproval before shipment.
Does every process adjustment need buyer approval?
No. Routine maintenance and low-risk process controls can follow the agreed supplier procedure. Changes that may affect approved product characteristics, evidence or contractual requirements need the defined notification path.
Does MSTFAB provide a complete automotive PPAP?
Only when the customer defines the required elements for the sheet metal scope. We can provide agreed samples and mechanical fabrication records; finished equipment, electrical validation and vehicle-system evidence are outside our scope.
Can an alternative hinge or latch be used temporarily?
Yes, if the buyer approves the comparison, validation, affected quantity and expiry. Temporary approval should not silently become the new permanent source.
Does changing a powder-coating supplier require a new FAI?
It may require a partial reapproval covering color, texture, thickness, adhesion, masking and affected fits. The scope should follow the risk and contract.
Who approves the completed electrical enclosure system?
The OEM or qualified integrator. MSTFAB supplies the drawing-based empty sheet metal shell and agreed mechanical evidence only.
Freeze the Approved Shell Before Repeat Orders Begin
Send the released model, drawings, hardware list, finish specification, CTQs and change-notification requirements. MSTFAB will review the mechanical enclosure scope and propose a practical first-article and revision-control handoff.
 WeChat Contact
 WhatsApp Me Directly