What is a Supplier Change Control (PCN) protocol for sheet metal fabrication?
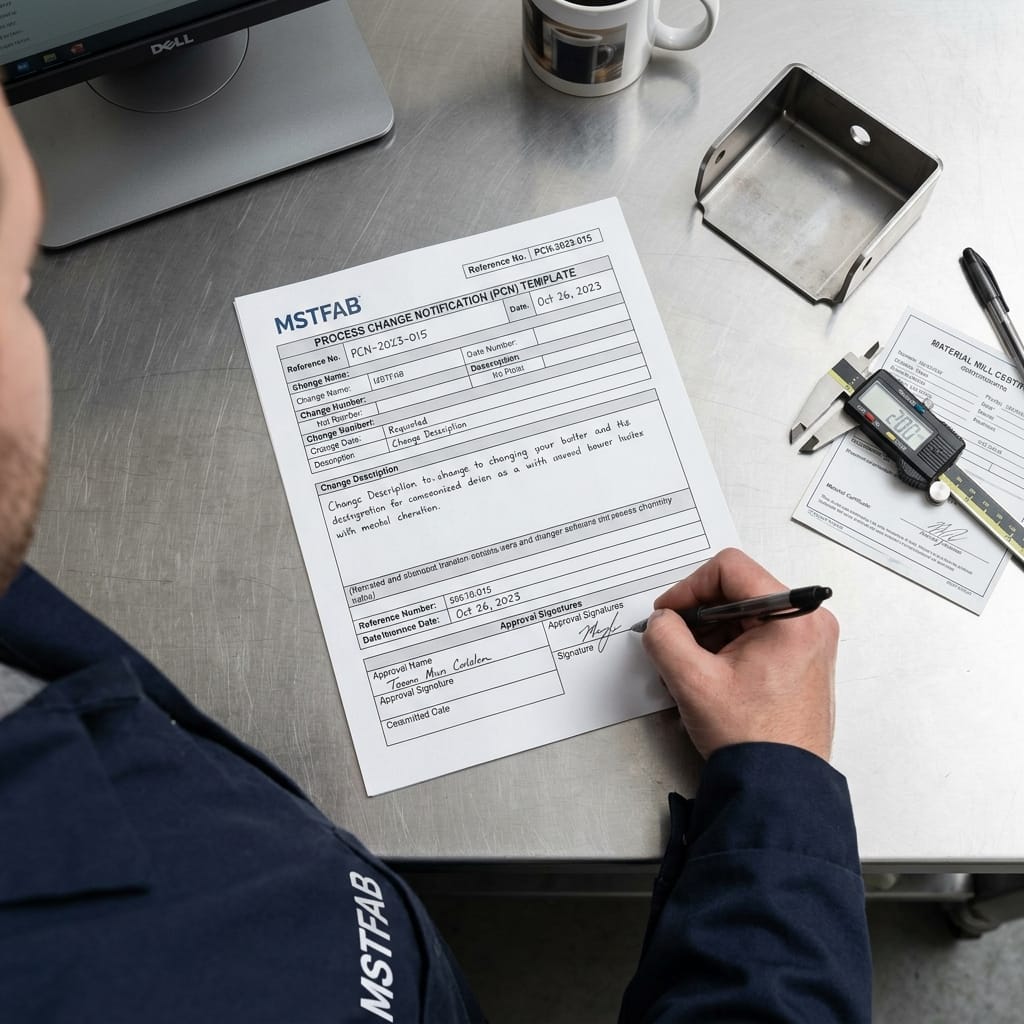
A Supplier Change Control (Process Change Notification or PCN) protocol is a legally binding quality framework requiring subcontract manufacturers to submit formal written documentation and technical validation data before altering any raw material sources, CNC machinery, forming tooling, sub-tier surface treatments, or plant production locations. The protocol prevents unauthorized production modifications and guarantees continuous product reliability.
In high-reliability industrial hardware, telecommunications, and medical enclosures, precision sheet metal fabrication is not a simple commodity trade. It is an interdependent manufacturing system comprising raw coil metallurgical properties, CNC cutting parameters, press brake tooling radii, automated welding setups, and multi-stage chemical pretreatment lines. When a supplier modifies any link in this chain without buyer authorization, the downstream assembly line faces catastrophic disruptions.
The 4 Pillars of a Robust Sheet Metal PCN Agreement
1. Clear Definition of “What Constitutes a Change”
Many suppliers assume that as long as final parts pass basic blueprint caliper checks, internal process adjustments do not concern the buyer. A legally enforceable Quality Agreement must clearly define triggered events:
- Raw Material Changes: Switching steel or aluminum mills, substituting temper designations (e.g., 5052-H32 to 5052-O), or altering sheet thickness tolerance tiers.
- Equipment Relocation: Transferring progressive stamping dies or CNC punch presses between facilities, sister plants, or distinct factory bays.
- Thermal & Cutting Parameters: Altering laser assist gases (e.g., nitrogen to shop air) or changing CNC punching stroke dynamics.
- Sub-Tier Outsource Transfers: Changing powder coating coaters, electroplating lines, or silk-screening sub-contractors.
2. Formal PCN Submission Workflow & Gatekeeper Timeline
A supplier must adhere to a standardized timeline before executing any manufacturing shift:
- Advance Notice Window (90 Days): Submit the formal PCN document at least 90 calendar days prior to the proposed production cutover date.
- Engineering Evaluation (15 Days): Buyer’s hardware and quality engineering team reviews data packages and determines requalification requirements.
- Sample Submission & FAI: Supplier produces a pilot run under proposed conditions and submits full First Article Inspection (FAI) reports.
- Sign-Off or Rejection: No parts produced under the new process can ship until a signed PCN approval document is uploaded to the buyer’s PLM system.

PCN Change Classification & Re-Qualification Requirements
The table below provides an industry-standard change control classification matrix for precision sheet metal components:
| Change Level | Fabrication Trigger Event | Advance Notice | Mandatory Validation Package | Buyer Approval Required? |
|---|---|---|---|---|
| Level 1: Critical | Manufacturing plant relocation, new primary stamping die, or raw material alloy change | 90 Days | Full Level 3 PPAP, 30-piece capability study (Cpk ≥ 1.33), environmental testing | YES – Written Consent |
| Level 2: Major | Secondary finishing vendor change, press brake replacement, or weld wire alloy shift | 60 Days | Delta FAI (affected features), cross-cut adhesion / weld macro-etch test, MTRs | YES – Written Consent |
| Level 3: Minor | Like-for-like CNC punch tooling regrind or preventive maintenance overhaul | 30 Days / Logged | Standard First-Piece Inspection report and internal maintenance sign-off log | Notification / Log Only |
| Level 4: Emergency | Tooling breakdown requiring temporary backup cell activation | Immediate (24 hrs) | Emergency deviation request, 100% manual inspection of all emergency lot parts | YES – Deviation Sign-Off |
Verification Technologies: Proving Equivalency
Trust but verify. When evaluating a supplier’s PCN submission, engineering teams deploy specialized physical and chemical verification tools:
- Positive Material Identification (PMI / XRF): Handheld X-ray fluorescence analyzers verify elemental compositions on-site in seconds, catching unauthorized alloy dilutions before parts reach the dock.
- Tooling Wear & Radius Analysis: Precision optical comparators and CMM probes measure punch and die working radii to guarantee forming geometries remain within tight CAD limits (±0.05 mm).
- Accelerated Environmental Stress: 500-hour ASTM B117 salt fog exposure and thermal cycling chambers test whether new powder coatings or plating pretreatments match baseline durability.

Partner With a Certified Sheet Metal Fabricator You Can Trust
MSTFAB operates under an uncompromised ISO 9001:2015 change management framework. We never alter materials, machines, or finishing chemistries without full transparency and pre-validated customer documentation. Connect with our engineering directors today for an audit-ready sheet metal quote.
 WeChat Contact
 WhatsApp Me Directly