⚡ Direct Answer: How to Specify and Source Custom Sheet Metal Channels?
Sourcing custom sheet metal channels (U-channels, C-profiles, Hat channels, J-trims, and sliding raceways) requires controlling 4 primary dimensional criteria: 1) Inside Channel Web & Leg Dimensions: Holding internal opening tolerances to ±0.25mm to ensure smooth mating with structural guide rollers or sliding modules; 2) Leg Flare & Angularity Control: Eliminating springback flare (keeping opposing channel legs strictly parallel at 90° ± 0.3° along the entire length); 3) Longitudinal Camber & Bowing Limits: Keeping channel camber under 1.0mm per meter using staged press brake bending and crowning compensation; and 4) Pre-Punched Mounting Patterns: Laser cutting slotted adjustment holes and cable tie-off louvers in the flat pattern prior to channel forming.
Custom Channel Profile Geometry & DFM Parameters
| Channel Profile Type | Typical Dimensional Ratio | Tooling Constraint | Primary OEM Function |
|---|---|---|---|
| Standard U-Channel | Web width W ≥ 1.5× Leg height H | Leg height limited by press brake punch throat depth | Structural equipment framing, cable raceways, protective edges. |
| C-Channel (Inward Lips) | Return lips L = 10mm–25mm | Requires segmented goose-neck punch to clear return lips | Heavy machinery uprights, captive slide tracks, wiring gutters. |
| Hat Channel (Outward Lips) | Flange width F ≥ 15mm for bolting | Formed in 4 successive bends; requires wide V-die spacing | Sheet metal panel stiffeners, acoustic damping, stand-off mounting. |
| Asymmetrical J-Channel | Unequal leg heights (e.g. 50mm vs 20mm) | Backgauge must register off web centerline or short leg | Enclosure drip shields, interlocking door seals, retainers. |
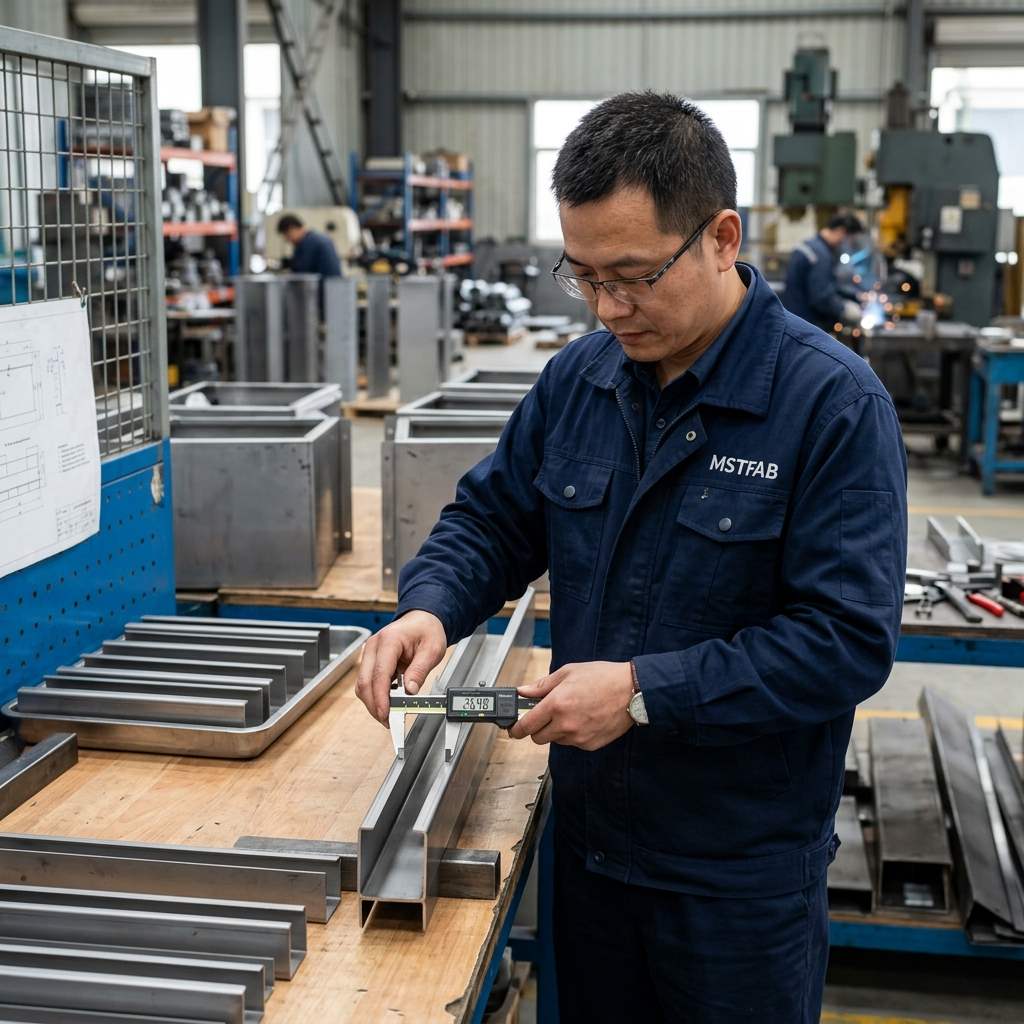
Custom roll-formed or press brake-formed channels are critical structural members in automation systems, power distribution racks, and conveying lines. Standard catalog extruded channels often lack the exact hole pitch or custom leg dimensions needed for proprietary OEM assemblies. MSTFAB manufactures custom channels up to 3 meters in length from carbon steel, galvanized steel, aluminum, and 304/316 stainless steel with zero dedicated tooling charges.

Leg Parallelism & Press Brake Tooling Staging
When bending deep channels where the leg height exceeds the web width, the newly formed first leg will collide with a standard straight punch body on the second bend. MSTFAB utilizes segmented, high-clearance goose-neck punches and windowed tooling setups, allowing deep U and C-profiles to be bent cleanly without deformation or tooling marks.

Need Custom Sheet Metal Channels Formed Up to 3 Meters?
Send your channel dimensions and hole patterns to MSTFAB. We provide rapid DFM analysis on press brake punch clearance, springback control, and surface finishing.
Frequently Asked Questions on Custom Channels
How narrow can the internal web of a U-channel be?
On a CNC press brake, the minimum inside web width must equal at least the minimum V-die opening required for the sheet thickness (typically 6× to 8× sheet thickness). For ultra-narrow channels, specialized acute punch tooling is required.
How do you prevent long channels from bowing longitudinally after forming?
Bowing is caused by residual rolling stresses in coil stock. We utilize laser stress-relief micro-tabs, calibrate CNC hydraulic crowning across the brake bed, and apply reverse pre-bending adjustments for channels longer than 2,000mm.
 WeChat Contact
 WhatsApp Me Directly