
How do design engineers and buyers compress custom sheet metal prototype lead times to 3–5 business days?
Achieving rapid 3-to-5-day turnaround for sheet metal prototypes requires: (1) designing around in-stock standard commercial materials (1.0 mm–3.0 mm cold rolled steel, 5052-H32 aluminum, and 304 stainless steel), (2) specifying standardized internal bend radii (r = 1.0t) matching in-rack press brake punches to eliminate custom tooling setup delays, (3) submitting production-ready 3D CAD models (STEP/IGES) paired with 1:1 DXFs to bypass CAM manual drafting, (4) replacing continuous full-penetration welds with self-fixturing tab-and-slot joint geometry or intermittent stitch welds, and (5) selecting fast-curing standard stock powder coat colors (RAL 7035, RAL 9005) or bare mechanical grain finishes.
1. The Race to Market: The Critical Need for Fast-Turn Prototypes
In modern hardware product development—whether launching medical diagnostic devices, telecommunications rack hardware, EV charging stations, or industrial robotics—speed to market is the primary competitive differentiator. Hardware engineers cannot afford to wait four to six weeks for prototype sheet metal chassis and brackets to validate mechanical fit-up, thermal airflow, and electromagnetic shielding (EMI).
However, “fast” must never mean “sloppy.” A quick-turn prototype that arrives out of square, with cracked bend corners or stripped PEM hardware, invalidates testing and halts assembly lines. Achieving high-speed turnaround without sacrificing production-grade dimensional fidelity requires a deliberate engineering approach aligned with factory tooling and material availability.
2. Rule 1: Specify In-Stock Standard Raw Materials
The number-one cause of prototype delays is calling out non-standard alloys, exotic tempers, or uncommon sheet gauges that require special mill orders. A mill run for an unusual thickness (such as 2.3 mm 6061-T4 aluminum) can easily add 3 to 4 weeks before fabrication even starts.
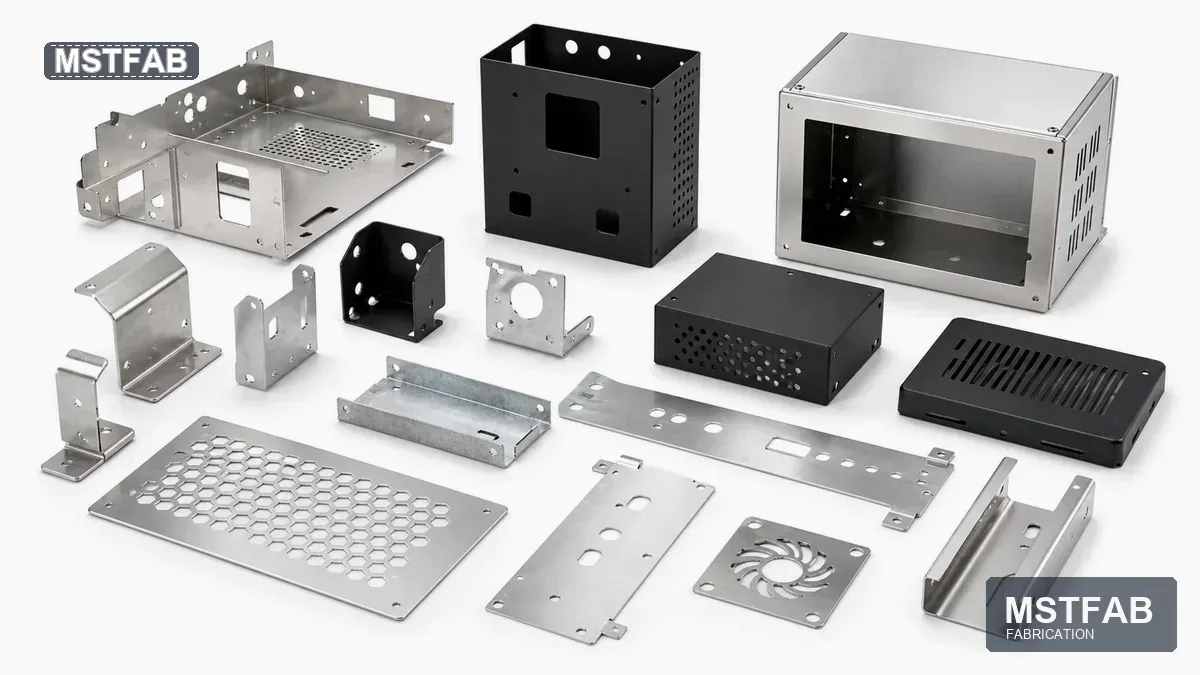
To guarantee 3-to-5-day turnaround, stick strictly to core stock alloys maintained in standard gauges (1.0 mm, 1.2 mm, 1.5 mm, 2.0 mm, 2.5 mm, 3.0 mm):
- Cold Rolled Mild Steel (ASTM A1008 CS Type B): Excellent formability, smooth surface finish, ideal for powder-coated chassis and brackets.
- 5052-H32 Aluminum: The supreme forming alloy. Does not crack during sharp bending, offers natural marine corrosion resistance, and is 65% lighter than steel.
- 304 / 304L Stainless Steel (ASTM A240, 2B or #4 Brushed): Corrosion-resistant, high tensile strength, ready for immediate use in food or medical environments without painting.
- Galvanized Steel (ASTM A653 G90): Pre-zinc coated steel offering instant rust protection for internal chassis and brackets with zero secondary finishing required.
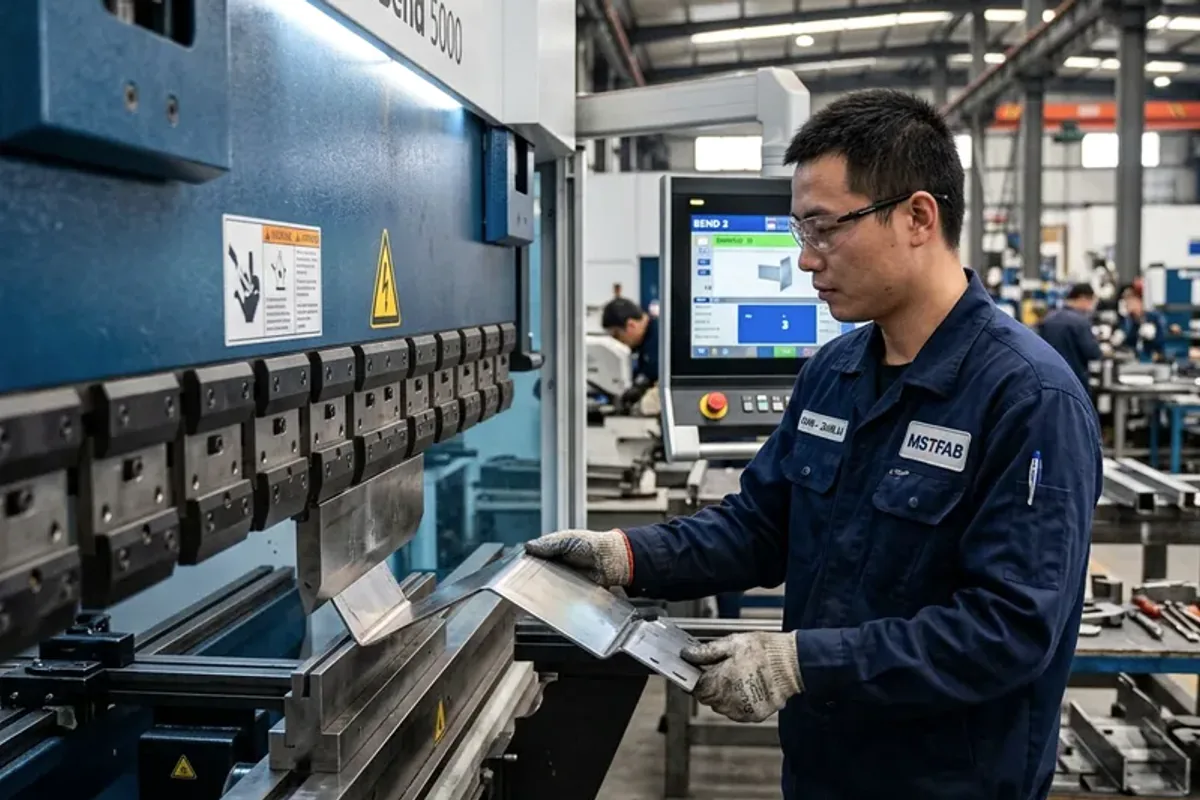
3. Rule 2: Design Around Standard Press Brake Tooling
Special bend geometries—such as tiny inside radii (< 0.5 mm), deep narrow channels with high aspect ratios, or custom rib profiles—require custom press brake tooling that takes weeks to order or grind.
For quick-turn manufacturing, adhere to standard press brake tooling geometry:
- Uniform Inside Bend Radius: Specify IR = 1.0t for steel and 1.0t to 1.5t for aluminum across ALL bends on the part. Using the same radius allows the press brake operator to complete all forming operations in a single machine setup without stopping to swap out punch segments.
- Standard Flange Heights: Ensure all return flanges meet the minimum V-die bridge threshold: hmin ≥ 4.0t. Flanges shorter than 4.0t slip into standard die openings, requiring special bottoming dies that slow down production.
- Standard Bend Reliefs: Always include rectangular or teardrop bend reliefs where a flange meets an unbent edge (relief width ≥ 1.0t, depth ≥ r + t).
4. Rule 3: Fast-Track Joining & Rapid Fixturing
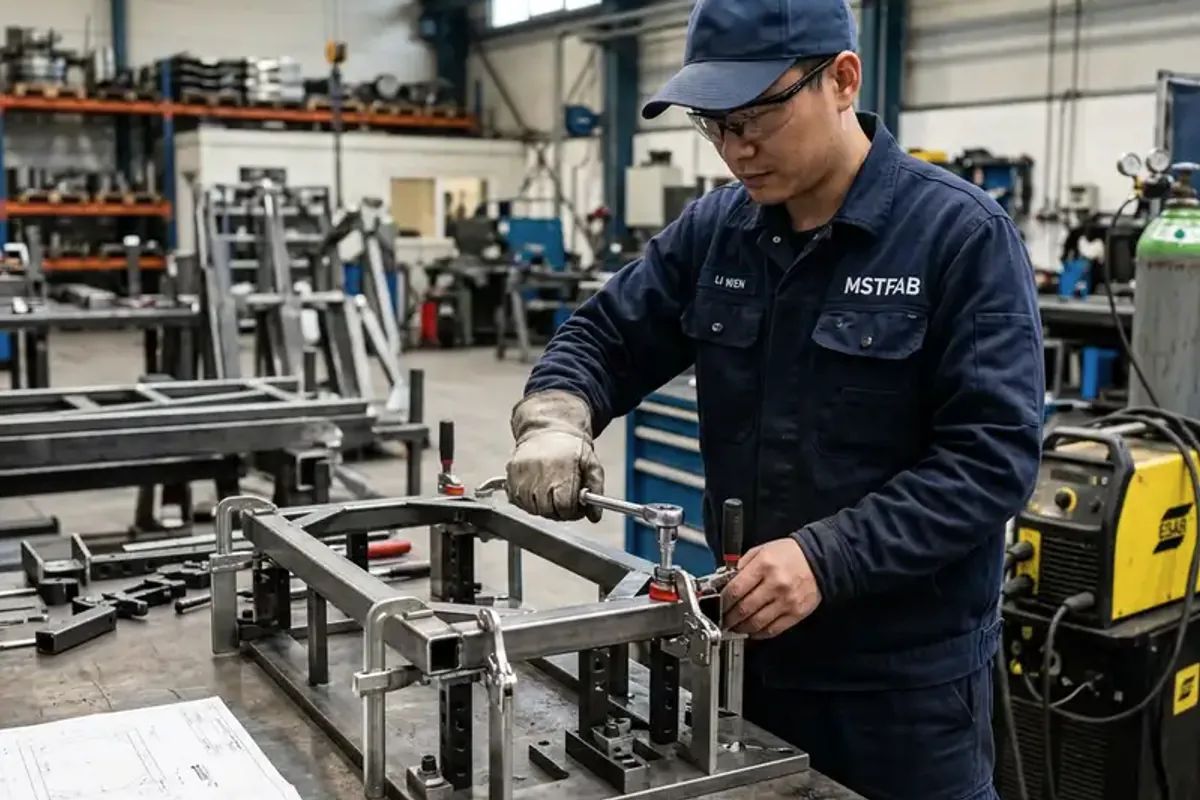
Designing complex welded enclosures that require dedicated hard steel welding fixtures is incompatible with quick-turn delivery schedules. Tooling fabrication alone takes 10 to 15 business days.
Instead, leverage Self-Fixturing Tab-and-Slot Joinery: laser-cut interlocking tabs and mating mortise slots locate mating panels mechanically in three dimensions (±0.05 mm repeatability). The assembly snaps together rigidly by hand, allowing the welder to tack and weld immediately on a modular 3D welding table without waiting for dedicated tooling.
5. Rule 4: Expedited Finishing Choices
Secondary finishing can easily consume more than 50% of the total manufacturing cycle time. Multistage anodizing, silk-screening, and custom color-matched wet paints add significant queue times.
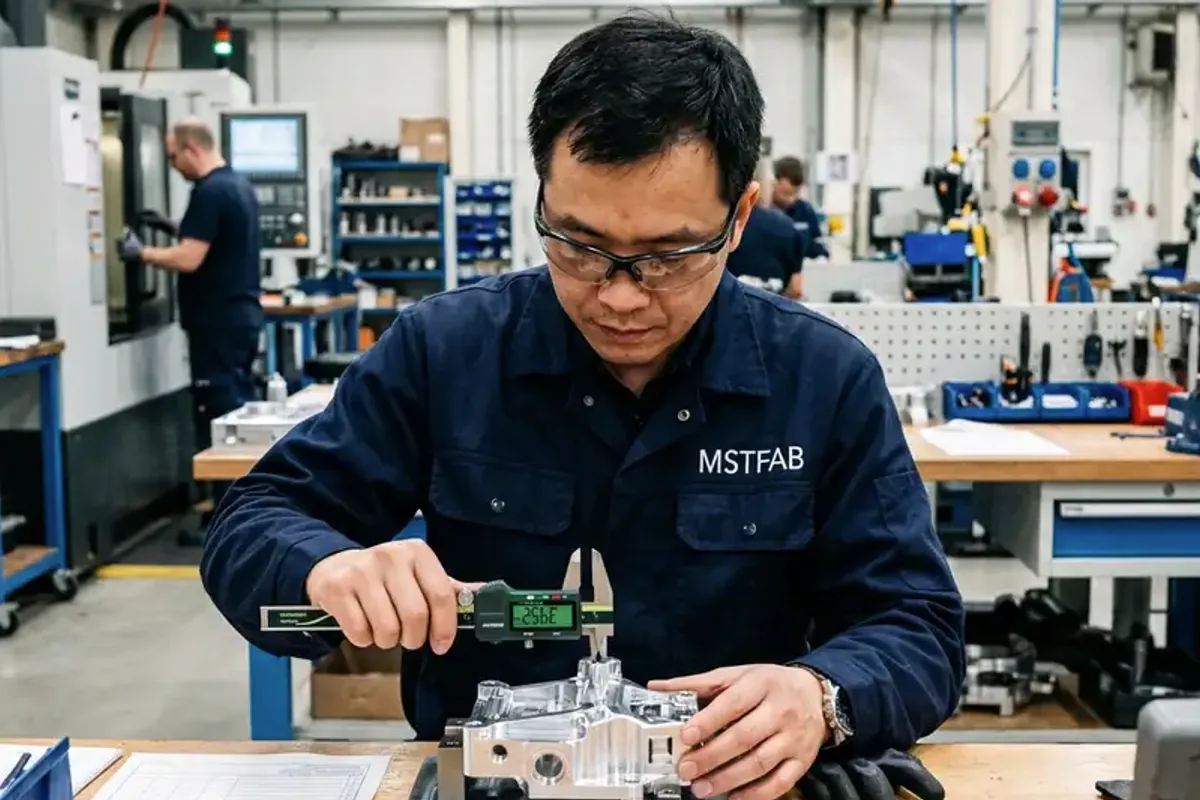
For fastest turnaround, select from these rapid finishing options:
- As-Fabricated / Deburred Finish (Lead Time: 0 Days): Clean laser-cut, deburred parts in galvanized steel, 5052 aluminum, or #4 brushed stainless steel ready for immediate mechanical fit-up testing.
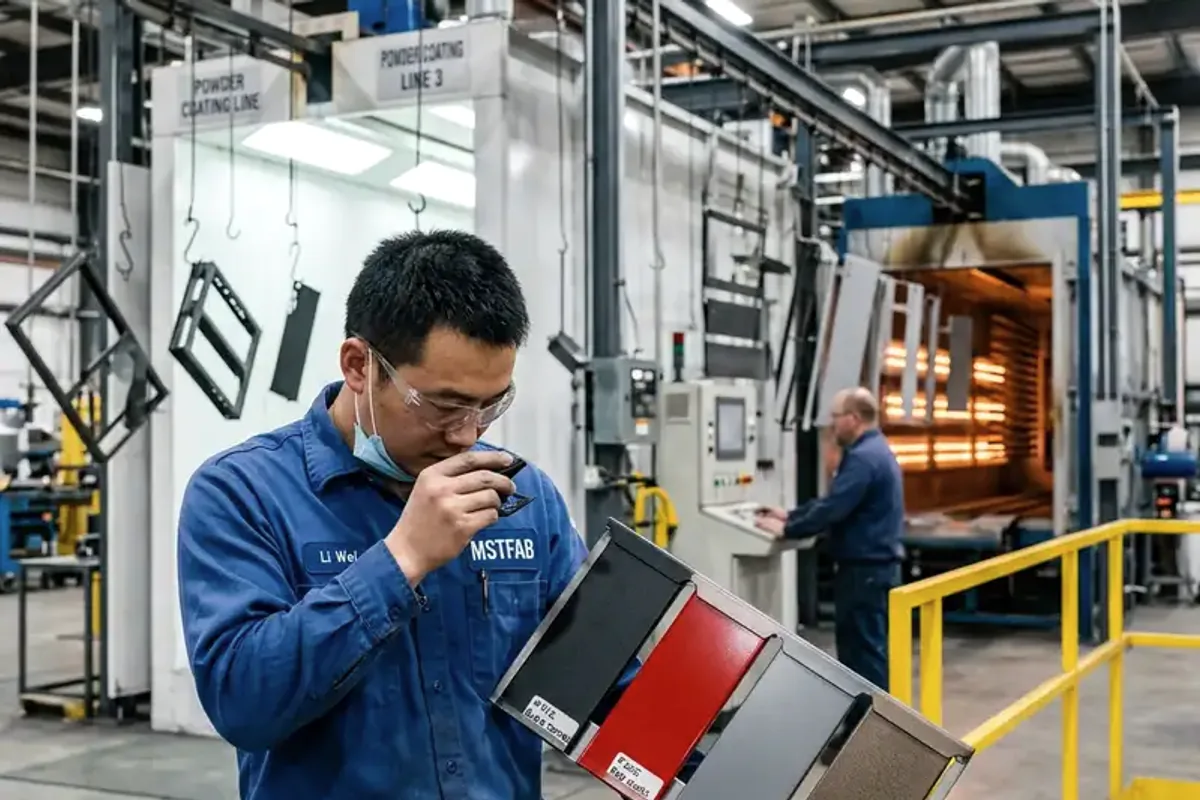
- Standard In-House Powder Coat (Lead Time: +1 to 2 Days): MSTFAB maintains dedicated electrostatic spray lines stocked with high-demand standard industrial colors: RAL 7035 (Light Grey), RAL 9005 (Jet Black, fine texture or semi-gloss), and RAL 9003 (Signal White).
- RoHS Clear Chem-Film (MIL-DTL-5541 Type II Class 3): Rapid automated dipping that provides aluminum corrosion protection and electrical grounding conductivity without paint curing delays.
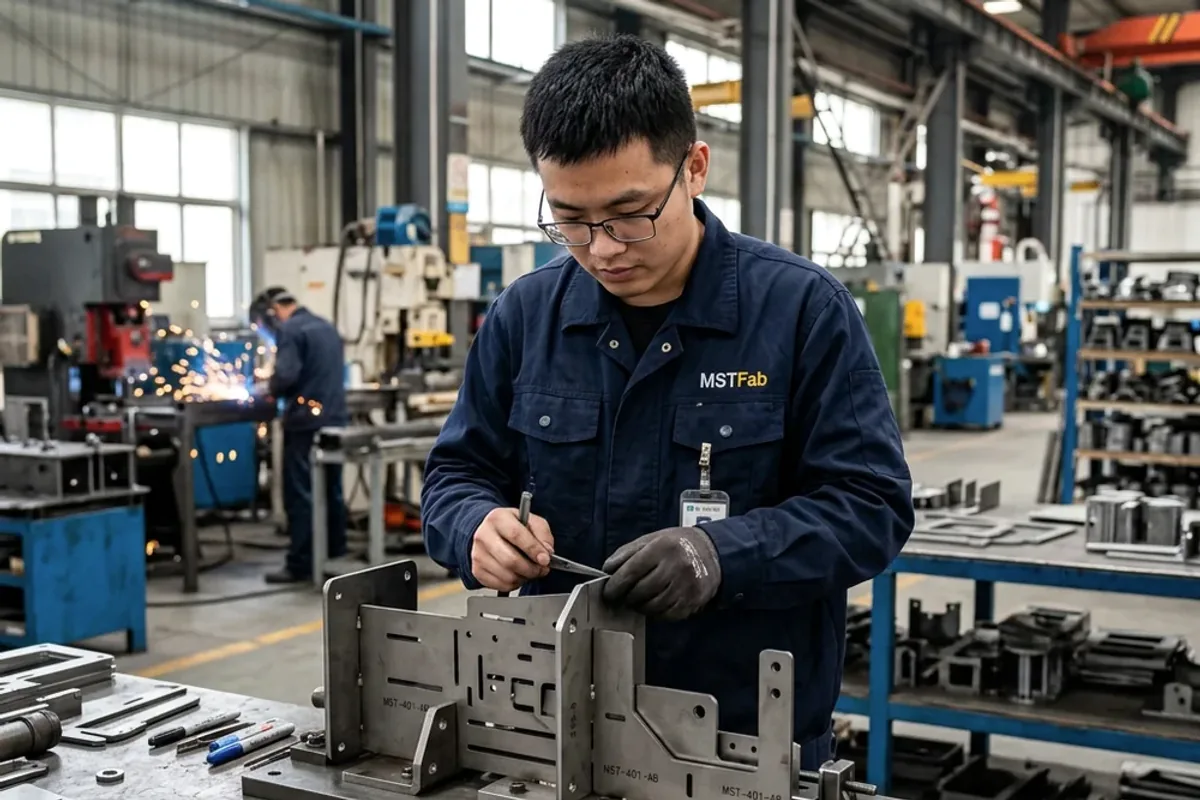
6. Quick-Turn Lead Time Planning Matrix
Plan your prototype schedules against MSTFAB standard operational lead times:
| Project Scope | Typical Operations Included | Expedited Turnaround | Standard Turnaround | Prerequisites for Speed |
|---|---|---|---|---|
| Flat Laser-Cut Blanks | Fiber laser cutting, wide-belt deburring | 24 to 48 Hours | 3 to 5 Days | Clean 1:1 DXF flat pattern; in-stock sheet |
| Formed Brackets & Panels | Laser cutting, CNC bending, PEM hardware | 3 to 4 Days | 5 to 7 Days | Standard bend radius (r = 1.0t); catalog PEM nuts |
| Welded Chassis & Frames | Laser, forming, TIG/MIG welding, blending | 4 to 6 Days | 7 to 10 Days | Self-fixturing tab-and-slot joint geometry |
| Powder-Coated Enclosures | Full fab + phosphating + powder coat | 5 to 7 Days | 10 to 14 Days | Stock RAL powder colors (RAL 7035, 9005, 9003) |
| Anodized / Chem-Film Parts | Full fab + MIL-DTL-5541 / Type II Anodize | 6 to 8 Days | 12 to 15 Days | Clear chem-film or clear natural anodize |
Need Production-Grade Sheet Metal Prototypes in Days?
Upload your 3D CAD models (STEP) and 2D DXF files. MSTFAB delivers rapid DFM feedback within 2 hours and ships precision laser cut, CNC bent, and powder-coated sheet metal prototypes in as little as 3 to 5 business days.
 WeChat Contact
 WhatsApp Me Directly